
Surface finishing · Partner plants we manage
Surface finishing managed from Vietnam: the finish menu our partner plants apply.
Saola Manufacturing manages electroplating, anodizing, gold and zinc plating, RoHS-compliant blue trivalent chromate, powder coating with pad printing and oil-dip rust protection through partner finishing plants — with salt-spray results supplied on request, not a marketing claim. It is a fixed menu of eight finishes, not a custom-chemistry shop. The quote names the production site and country of origin.
- Purchase order
- 1
- Machining and finishing on the same order
- Finishes
- 8
- Coatings and platings applied by partner plants
- Hours
- 48
- Quote returned from your drawing
- RMS
- 125
- Substrate finish expected before plating
01 — What we actually offer
A fixed menu, not a custom-chemistry shop.
We manage eight finishes through partner plants, applied to parts machined at our lead CNC plant or sourced from the casting and stamping partners we manage. If your drawing calls for something outside this menu, tell us early — we would rather say no than improvise a coating that has not been qualified.
The menu
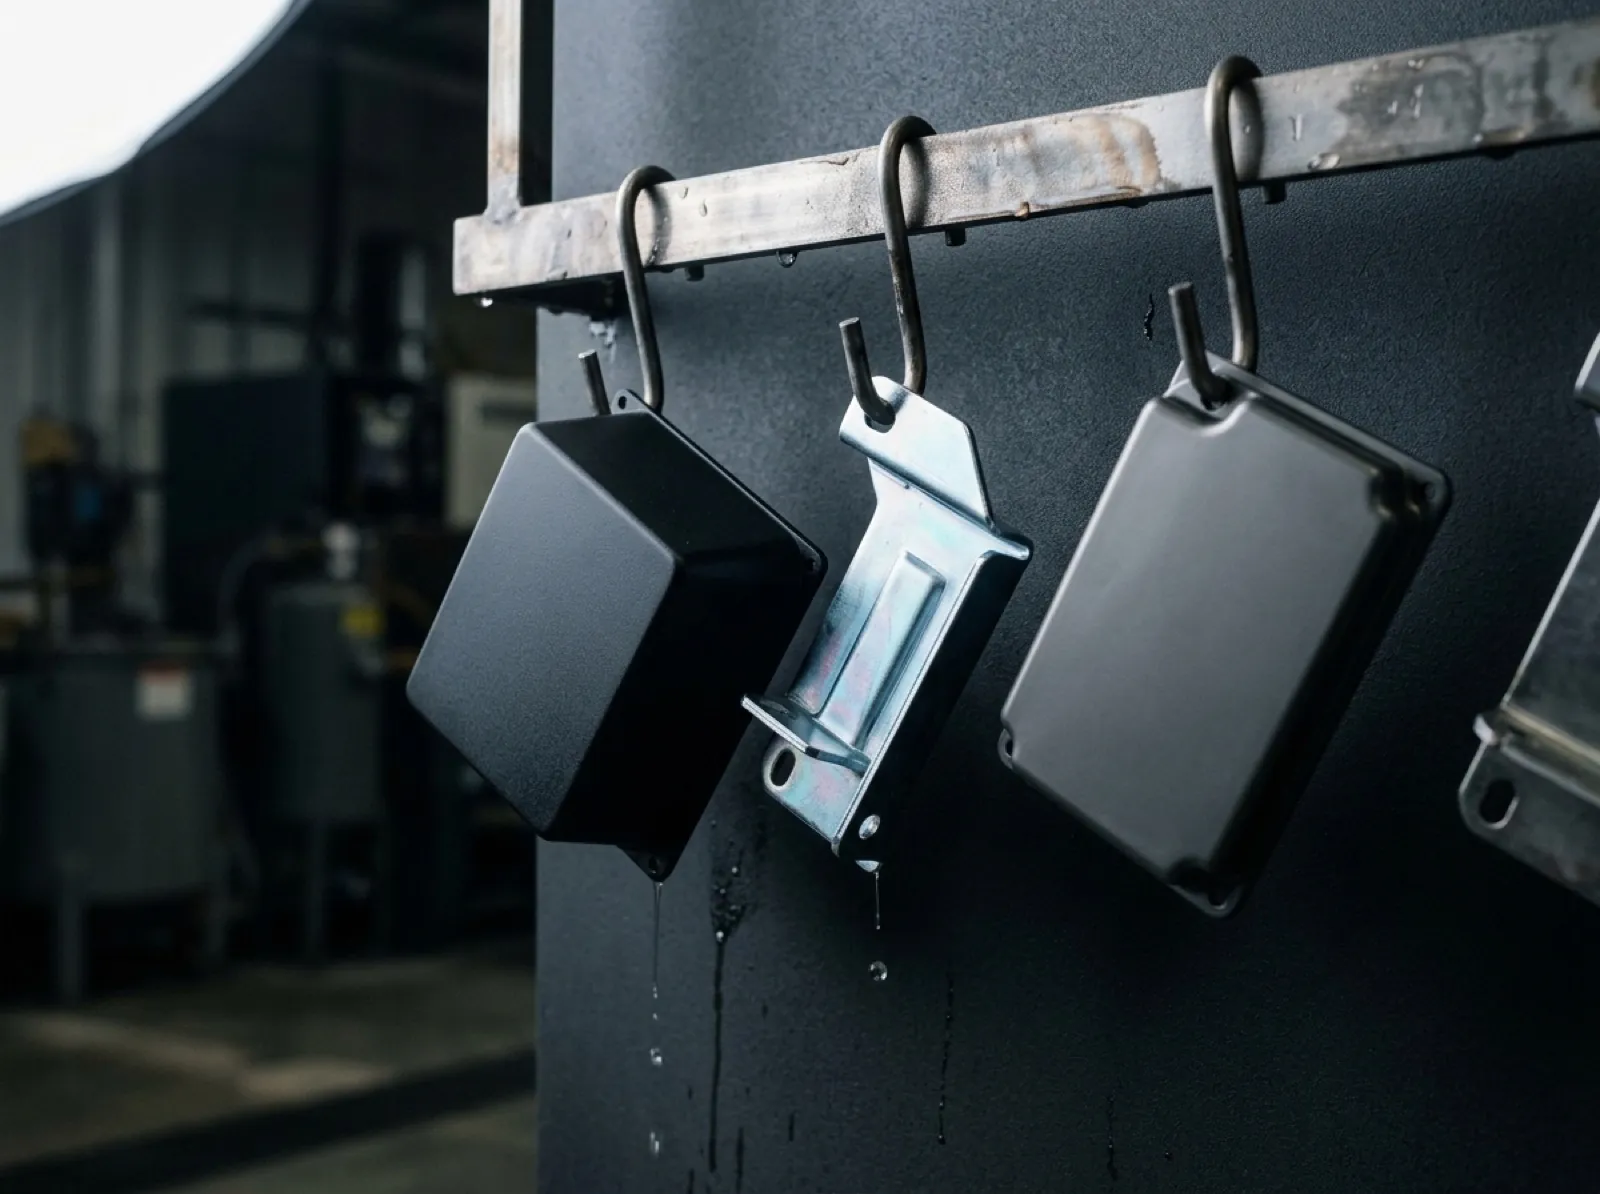
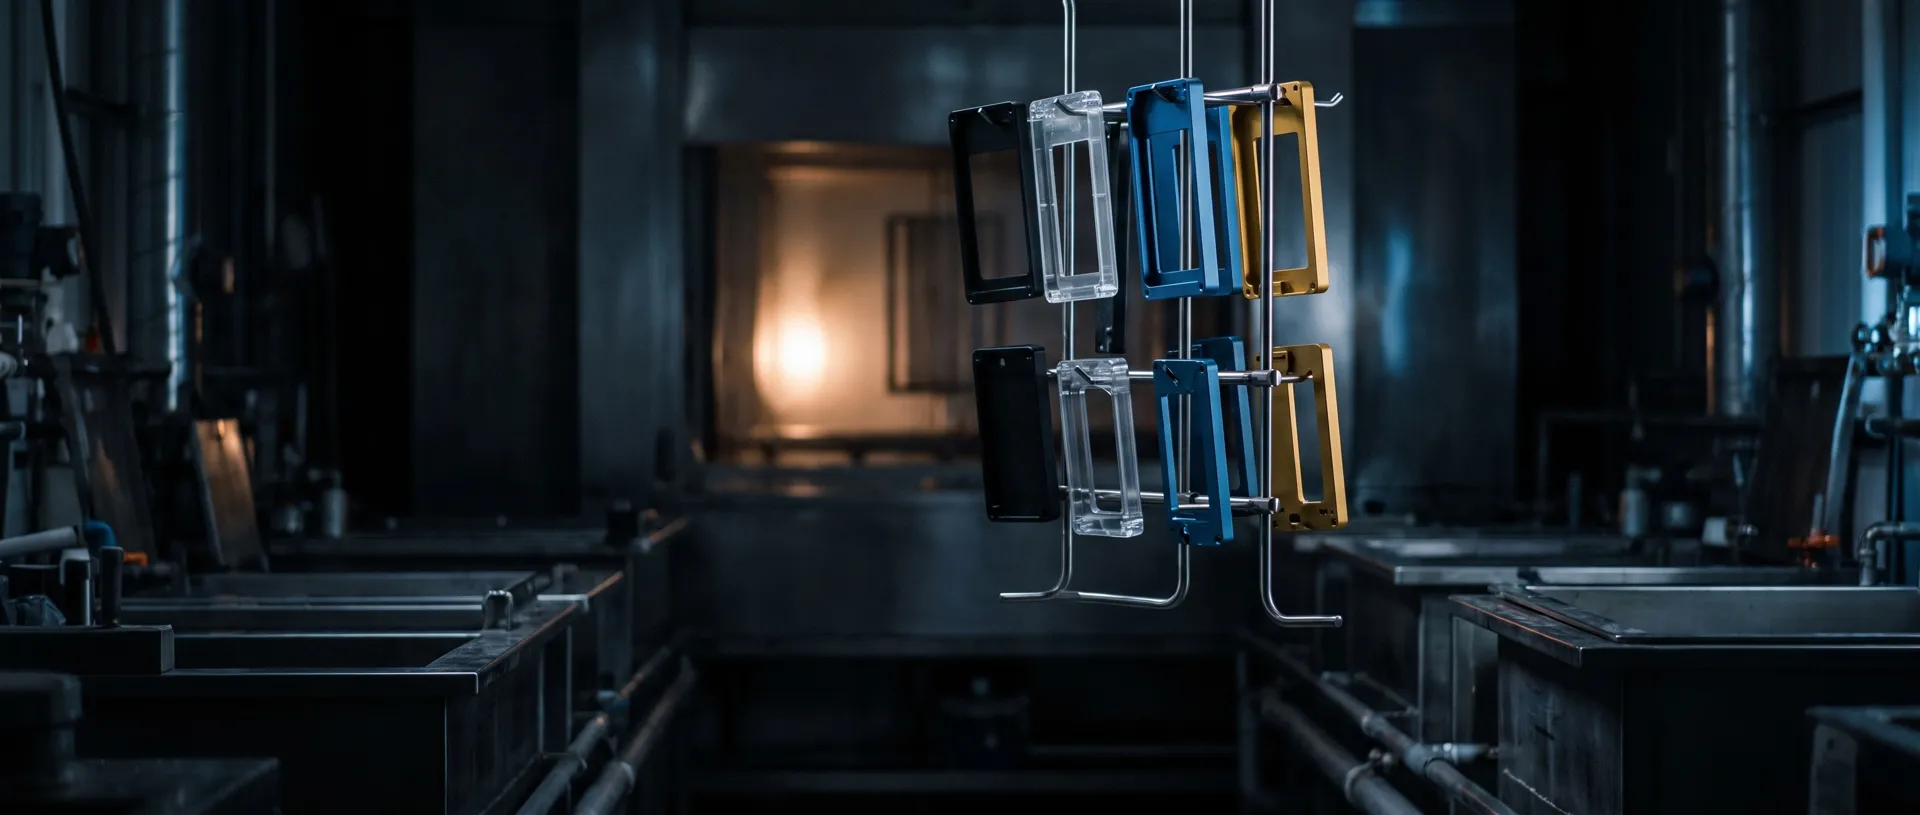
Corrosion protection: zinc plating, RoHS-compliant blue trivalent chromate, oil-dip rust protection, anodizing on aluminum.
Cosmetic and decorative: electroplating, gold plating, powder coating, pad printing for part markings and logos.
Finishes by industry: powder coat on gas and water distribution housings, and cosmetic coatings on medical, dental and veterinary equipment. Sourcing finished parts out of China? Read how US tariffs and country of origin apply to cast and machined parts.
Choosing between them? The guide to anodizing vs powder coating vs zinc plating compares base metals, coating thickness by standard, dimensional growth and drawing callouts.
Tapped holes on an anodized or plated part? Read why threads bind after anodizing or plating. Choosing between electroplated zinc and hot-dip? Read zinc plating vs galvanizing. Powder coating die-cast aluminum? See how to avoid outgassing blisters.
02 — Process parameters
The whole menu, by category.
If a finish is not on this list, we do not offer it today.
| Category | Options |
|---|---|
| Platings | Electroplating, gold plating, zinc plating, RoHS-compliant blue trivalent chromate |
| Coatings | Anodizing on aluminum, powder coating |
| Marking | Pad printing |
| Corrosion treatment | Oil-dip rust protection |
| Salt-spray performance | Test standard and duration confirmed in the quote |
| Substrate finish expected before plating | 125 RMS |
| Where each step is done | Machining before finishing at our lead CNC plant · every finish above at a partner plant; the quote names the production site and origin |
03 — Take cost out of the drawing
Where finishing cost actually comes from.
Finishing cost is driven by racking, masking and changeovers more than by the coating itself. These are the call-outs that keep it simple.
1. Name the exact finish, not a generic category
"Plated" is not a specification. Call out zinc plating, RoHS-compliant blue trivalent chromate, or whichever finish on our menu you actually need — a generic call-out forces a clarification round before we can quote at all.
2. Mark what must stay bare
Threads, ground contacts and press-fit bores usually need to stay free of coating. Call these out explicitly so they are masked correctly the first time, instead of discovering a fit problem on incoming inspection.
3. Reserve cosmetic-class call-outs for visible faces
A tight cosmetic-acceptance standard on a face nobody will ever see adds inspection time for no benefit. Tell us which faces are cosmetic and which are functional.
4. Lock pad-print artwork before the first production run
A logo or part-marking change after tooling means re-running the pad-print plate. Finalize artwork at the same time as the drawing, not after first samples ship.
5. Group a multi-part order by finish family
Every finish change is a tank or booth changeover. If your order has several part numbers, grouping them by finish rather than by assembly keeps them moving through fewer changeovers.
04 — Where this is the wrong process
What surface finishing does not do here.
Eight finishes, and only those eight
We do not offer decorative chrome-look plating, specialty conversion coatings, or any finish outside the menu above. Salt-spray test standard and duration are confirmed in the quote; we do not claim results beyond what the test report shows.
If your specification requires a finish or a test standard we do not offer, say so before tooling. We would rather route you correctly than take an order we cannot finish to print.
05 — One supplier, one PO
Finishing is the last stop for every process we manage.
Whatever comes off the lathe or mill at our lead CNC plant, or from a partner mold, press or flask, goes to a partner finishing plant before it is packed.
Die casting
Powder coat or plate the casting machined at our lead CNC plant, at a partner plant, before it ships.
See die castingCNC turning
Zinc plating or RoHS trivalent chromate applied by a partner plant to turned bushings and shafts.
See CNC turningStamping
Deburred, oil-dipped or plated brackets and clips, finished by partner plants after the press.
See stampingCNC milling
A casting machined at our lead CNC plant moves to a partner plant for plating or coating on the same order.
See CNC millingSand casting
Polishing at our lead CNC plant and plating at a partner plant for brass and bronze valve bodies.
See sand casting
What does the salt-spray result actually mean?
It records how the finish performed in a salt-spray corrosion test before base-metal corrosion broke through. The test standard and duration for your part are confirmed in the written quote, and we do not claim performance beyond what the report shows.
What is RoHS-compliant blue trivalent chromate?
A zinc-plating topcoat that adds corrosion resistance without the hexavalent chromium that RoHS restricts. It is our standard chromate finish, and it is what we quote unless your drawing calls out something else.
Can Saola finish parts that were made elsewhere?
Usually, if the incoming parts pass our inspection for surface condition and material. A partner plant applies the finish; send a sample and the finish spec and we will confirm before quoting.
Surface finishing guides
Send a finish spec. See what comes back.
STEP or PDF, with the finish called out. You get a unit price at your volume, the lead time, and a short note on anything we would change to take cost out.