
Bushings & bearing sleeves
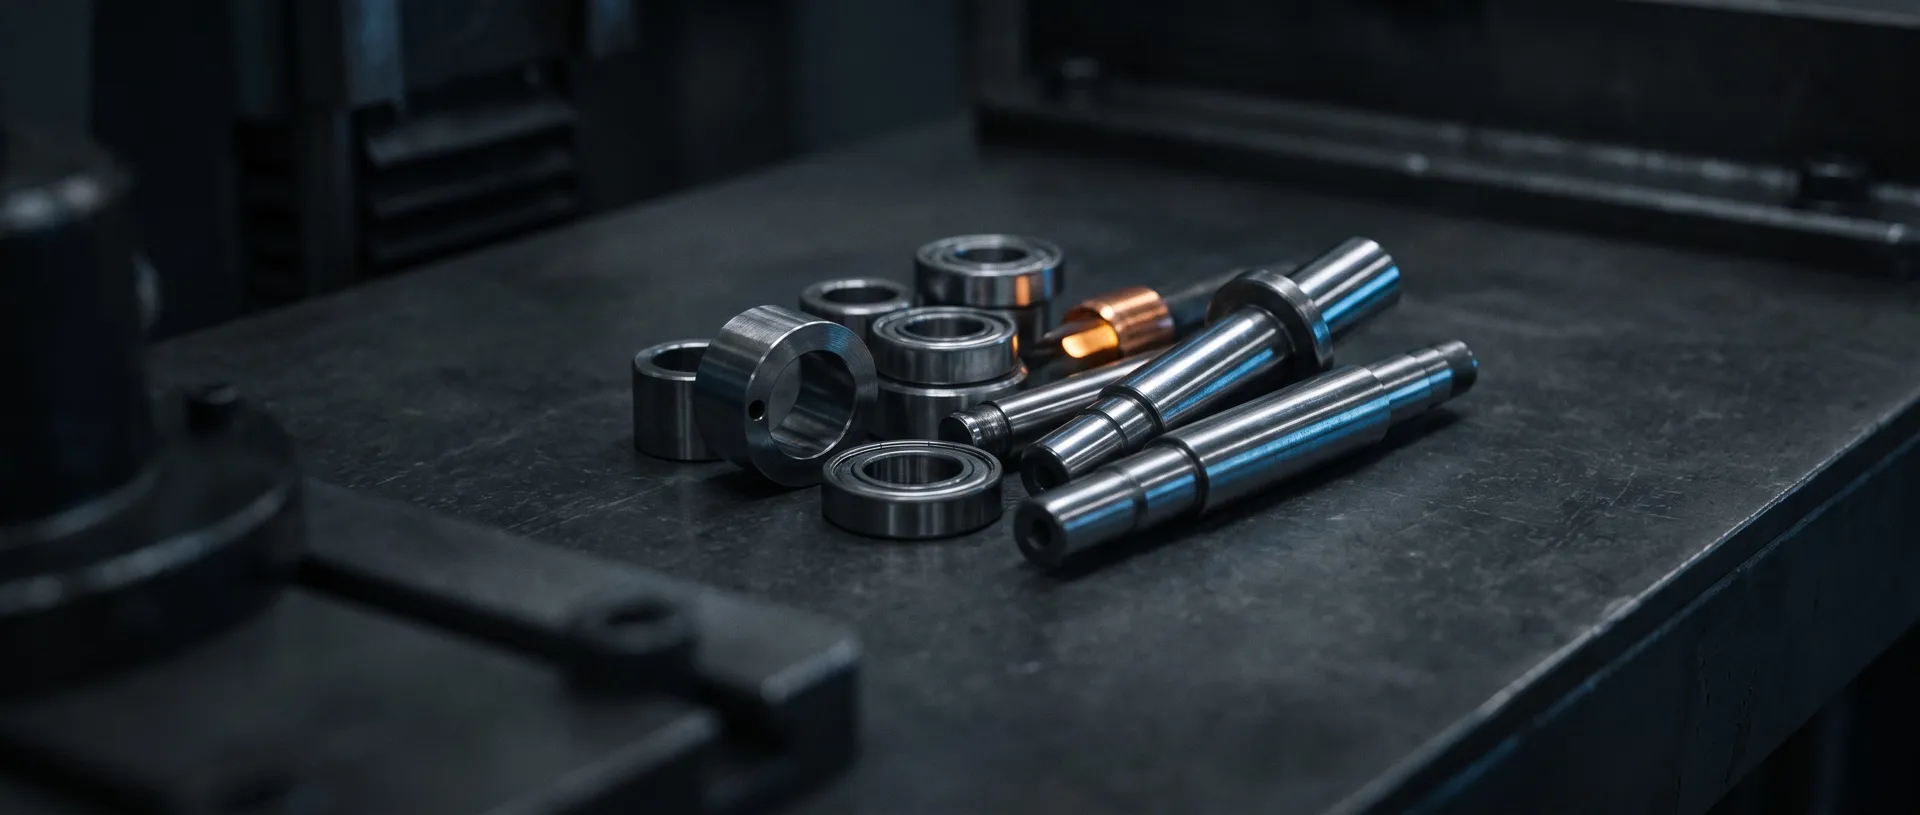
Turned from silicon bronze or 52100 steel bar, held to a running fit against a shaft or pin, polished on the bore.
Machine tool & industrial equipment · Machined in Vietnam
Bushings, eccentric rings, spacers, shafts and silicon-bronze wear parts for spindles, fixtures and drive assemblies. The material callout, the bore concentricity and the surface finish are called out tightly, and we hold them. A loose fit shows up as vibration, not a rejected part.
01 — The parts we make for this industry
These parts sit inside the machine, not on the outside. Nobody is grading them on looks — they are graded on whether the assembly runs true.
Turned from silicon bronze or 52100 steel bar, held to a running fit against a shaft or pin, polished on the bore.
Turned and milled in 12L14 or C1117 steel, offset bores held on center, keyways cut to print for a positive drive.
Die cast in ADC12 aluminum at a partner foundry, machined at our lead CNC plant for the bearing bore and mounting face, then powder coated by a partner plant; ADC12 is not a good anodizing alloy.
Turned from 52100 steel or aluminum 2011-T3, keyed or knurled where the drawing calls for a press or set-screw fit.
Stamped by a partner plant or milled at our lead CNC plant from aluminum 6061-T6, anodized or powder coated by a partner plant depending on the exposure inside the machine enclosure.
Cast by a partner foundry we manage, then machined at our lead CNC plant, for slide ways, worm gears and other low-friction contact surfaces that see continuous cycling.
02 — What actually matters on these parts
None of these show up on a visual inspection. They show up as noise, heat or premature wear three months after the machine ships.
Machined bores on castings hold ±0.025 mm with GD&T concentricity to Ø0.003 in. A bore off axis by even a little loads a bearing unevenly and shortens its life.
125 RMS is the standard as-machined finish on running and mating surfaces; a finer finish for a bearing or seal face is set on your print and confirmed in the quote. A rougher finish on a bushing bore or a sliding face wears the mating part faster than it should.
A print calling for 52100, C1117, 12L14, 2011-T3, 6061-T6 or silicon bronze chose that alloy for a reason. It comes down to hardness, machinability or wear resistance, and we run the material on the drawing, not a lookalike.
Turned-feature tolerance is confirmed against your drawing in the written quote. If a shaft or bushing fit is critical, put the tolerance on the drawing before tooling and we will say plainly whether we can hold it.
03 — Typical routing by part family
Process route, material and finish for the part families above, with each step marked lead CNC plant or partner plant. Confirmed against your drawing before quoting; the quote names the production site and origin.
| Part family | Process route | Material | Finish |
|---|---|---|---|
| Bushings & bearing sleeves | CNC turning (lead CNC plant) | Silicon bronze / steel 52100 | Polish (lead CNC plant), oil-dip rust protection (partner plant) |
| Eccentric rings & spacers | CNC turning + milling (lead CNC plant) | 12L14 steel / C1117 steel | Zinc plating (partner plant) |
| Motor / gearbox covers & housings | Die casting (partner foundry) + CNC milling (lead CNC plant) | ADC12 aluminum | Powder coating (partner plant) |
| Drive shafts & collars | CNC turning (lead CNC plant) | Steel 52100 / aluminum 2011-T3 | RoHS blue trivalent chromate (partner plant) |
| Structural brackets | Stamping (partner plant) / CNC milling (lead CNC plant) | Aluminum 6061-T6 | Anodizing, powder coating (partner plant) |
04 — One part, one supplier
A representative routing for this industry. Turning, milling and polishing happen at our lead CNC plant, so the tolerance chain is set once; plating is done by a partner plant, and the quote names each site.
Silicon bronze or steel bar turned to the outer profile and the offset bore center at our lead CNC plant.
Keyway and secondary features cut to print at our lead CNC plant, bore concentricity checked in the same setup.
Running surfaces machined to 125 RMS as standard and polished at our lead CNC plant, finer where the print calls for it; plating or oil-dip treatment at a partner plant for the service environment.
Dimensional and GD&T check against print, individual bagging, cartons under 30 lb; the quote names where this is done.
05 — Where we are the wrong shop
Complex contoured features cut in one setup on a five-axis machine are outside what we run. If your part needs that, we will tell you on the first call, before any tooling is committed.
Turned-feature tolerance is confirmed against your drawing in the written quote. If a fit is very tight, put it on the drawing and we will tell you plainly whether we can hold it.
We run 52100, C1117, 12L14, 2011-T3, 6061-T6, silicon bronze and a small set of others. A print calling for something outside that list needs a separate sourcing conversation before we quote. Tell us early, not after the drawing is finalized.
06 — Before you send a drawing
Short answers here; the rest on the FAQ page.
Yes. Bores machined into castings at our lead CNC plant hold ±0.025 mm with GD&T concentricity to Ø0.003 in, checked at final inspection against your callouts.
Yes — the blanks are sand cast by a partner foundry we manage, then machined and inspected at our lead CNC plant.
Then we are the wrong shop for that feature, and we will say so directly rather than quote something we cannot hold. Ask us for a referral if that is the only blocker.
STEP or PDF, one part or a whole family. You get a unit price at your volume, the tooling cost and the lead time. We also flag any fit or material callout worth a second look. Turnaround is 48 hours.