
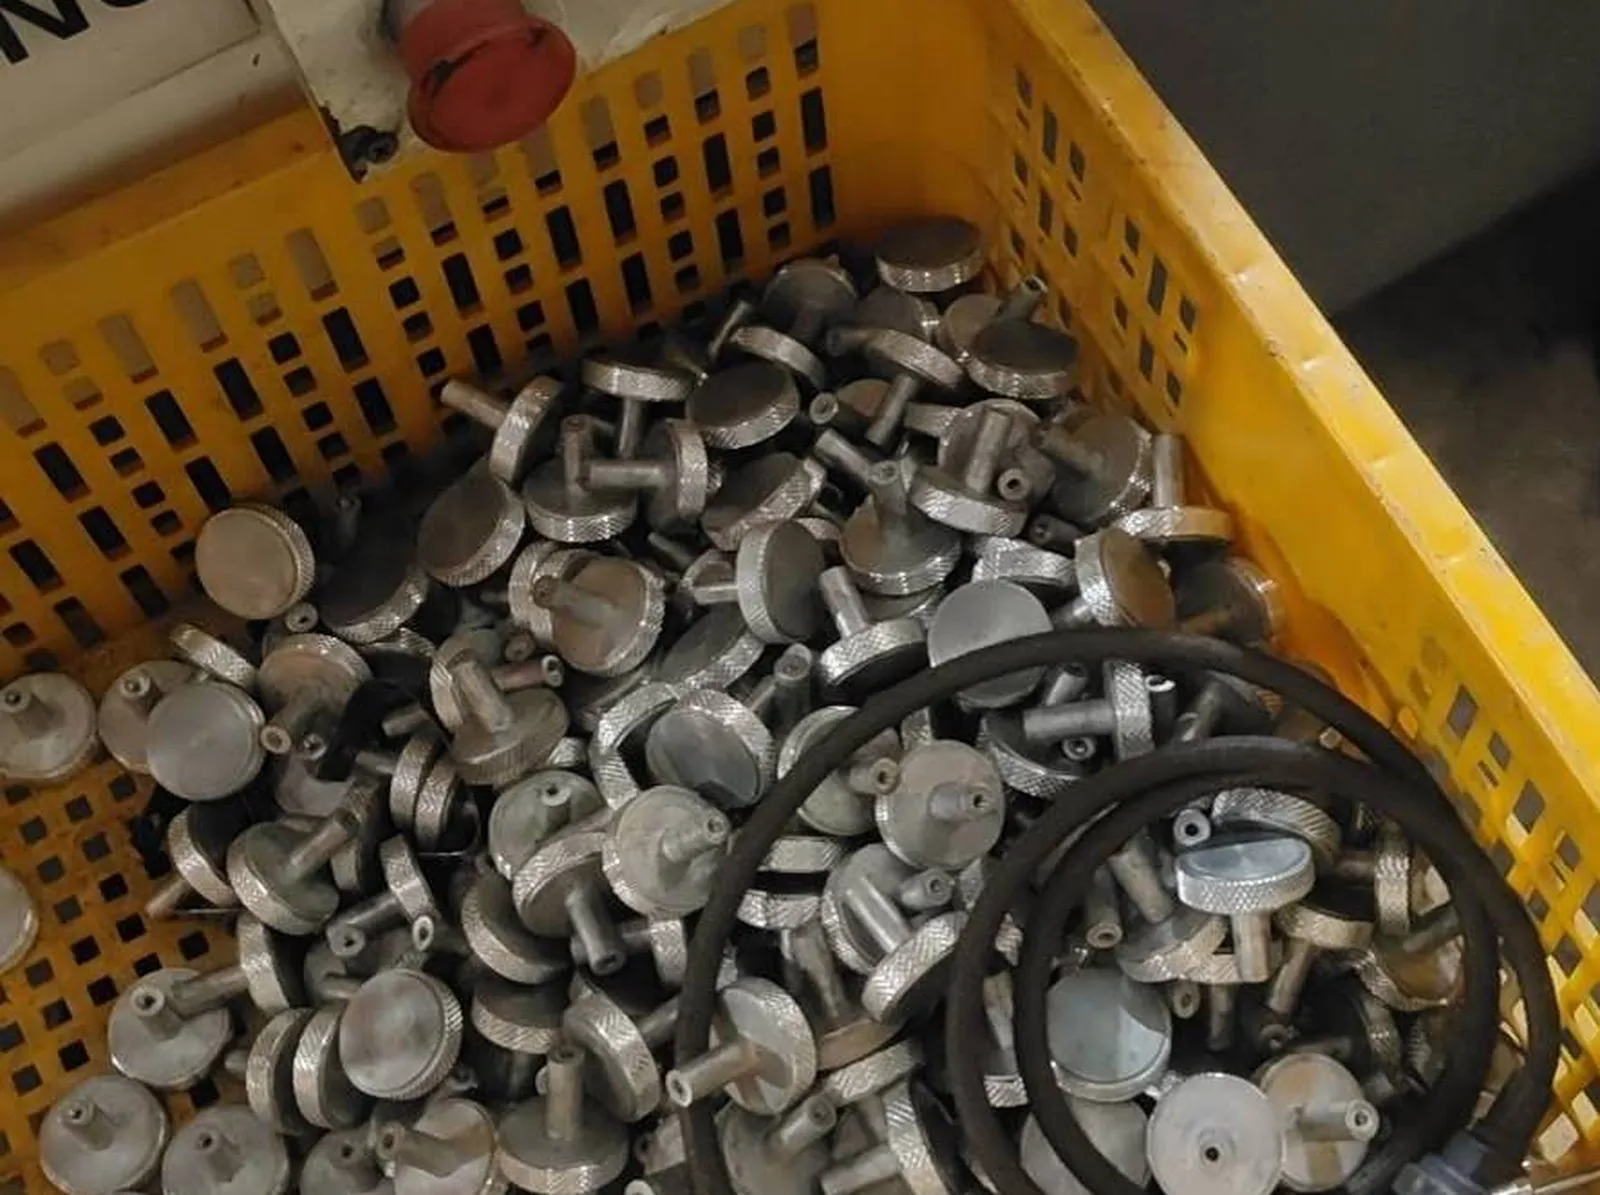
In-house
CNC Turning
Bar and tube work on CNC lathes: bushings, caps, inserts, shafts, knurled and threaded features.
ANPT/NPT to ASME B1.20.1 · knurling
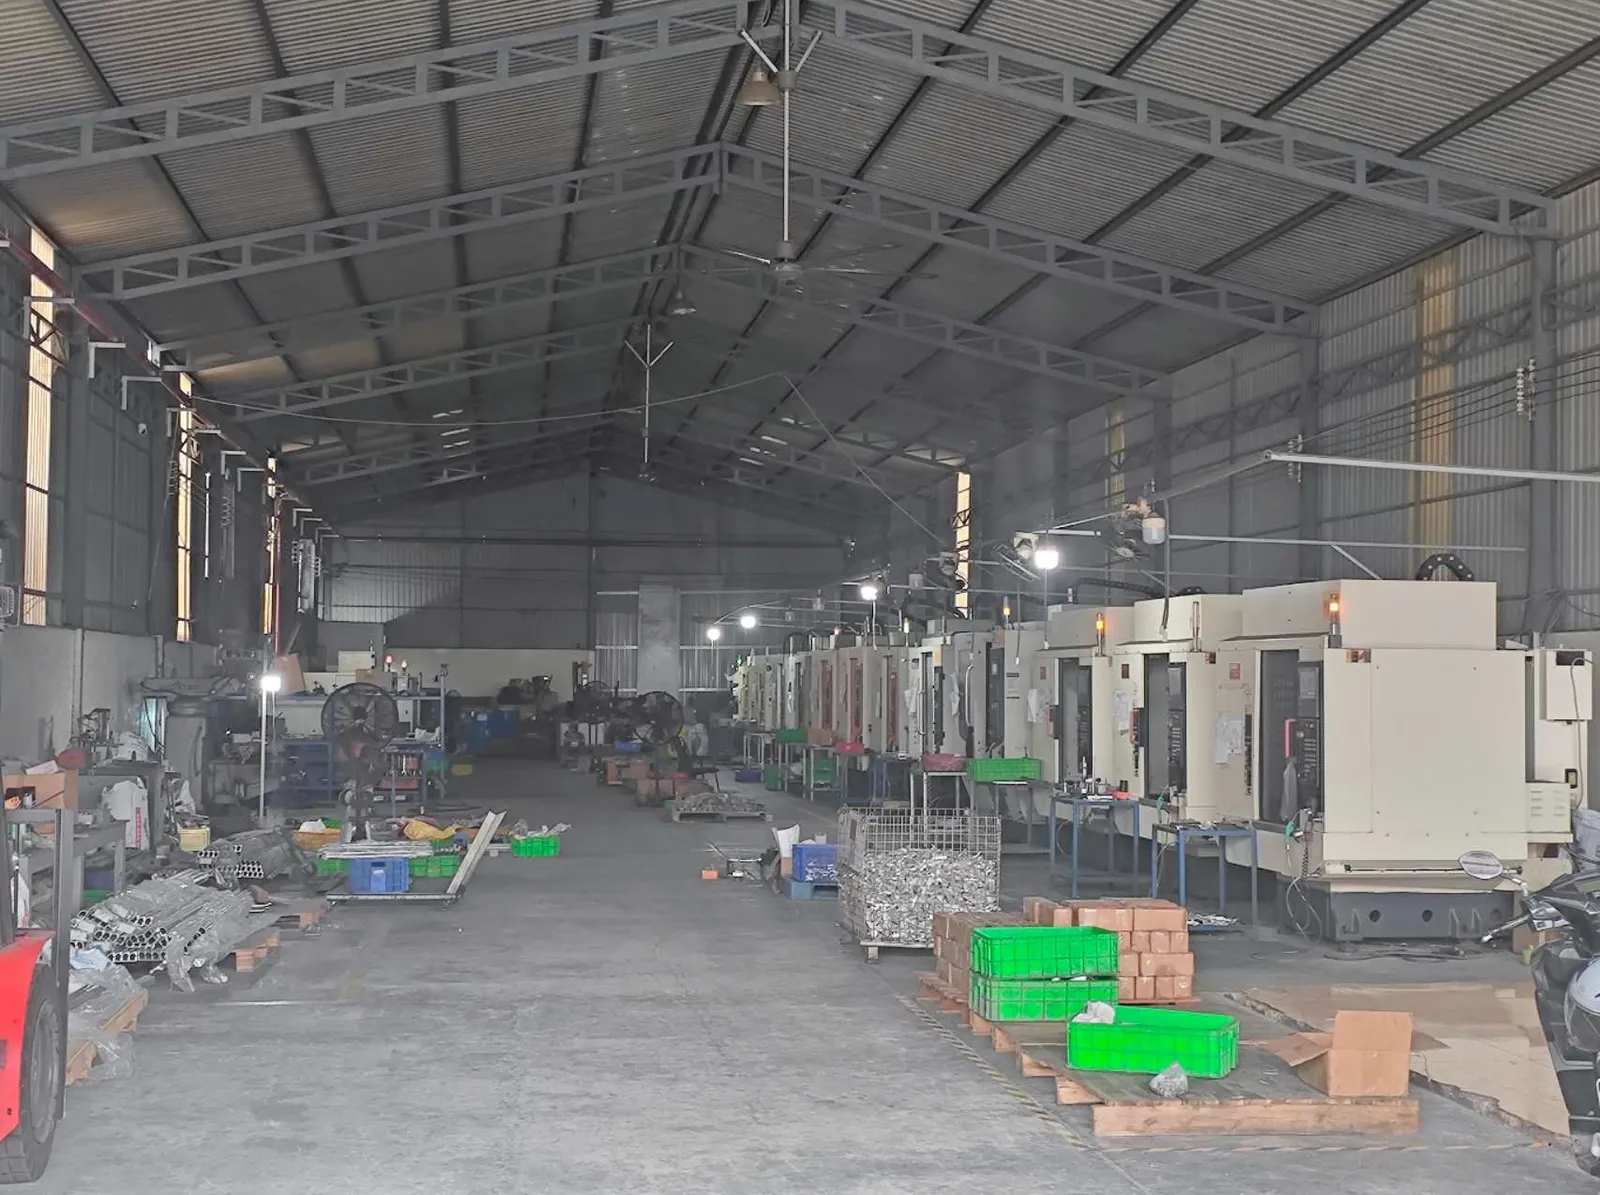
The lead CNC plant · former Binh Duong Province
Saola Manufacturing is the brand of Aximora Global Trading Co., Ltd., which places and manages metal-parts work in Vietnam. Our CNC work runs at our lead partner plant, T.K Viet Nam Precision Company Limited: founded 2017, family-held, with its own CNC turning and milling floor. This page shows that plant.
01 — Who we are
We are small on purpose and small in fact. Here is what that buys you, and what it costs you — we would rather you weigh both before you send a drawing.
You deal with the owner and the plant, not a layer of account managers between you and a decision.
We can shift a production schedule or run a smaller pilot batch without three levels of internal approval.
If something needs to change on a running job, the person who can change it is reachable directly.
If that is a hard requirement for your approved-vendor list, we are not the right fit yet, and we would rather say so now.
ISO 9001 is not yet issued. See quality & inspection for exactly what we can send today instead.
Early relationships with us won't come with years of case studies behind them. They will come with the owner answering your questions directly.
02 — What our lead CNC plant runs
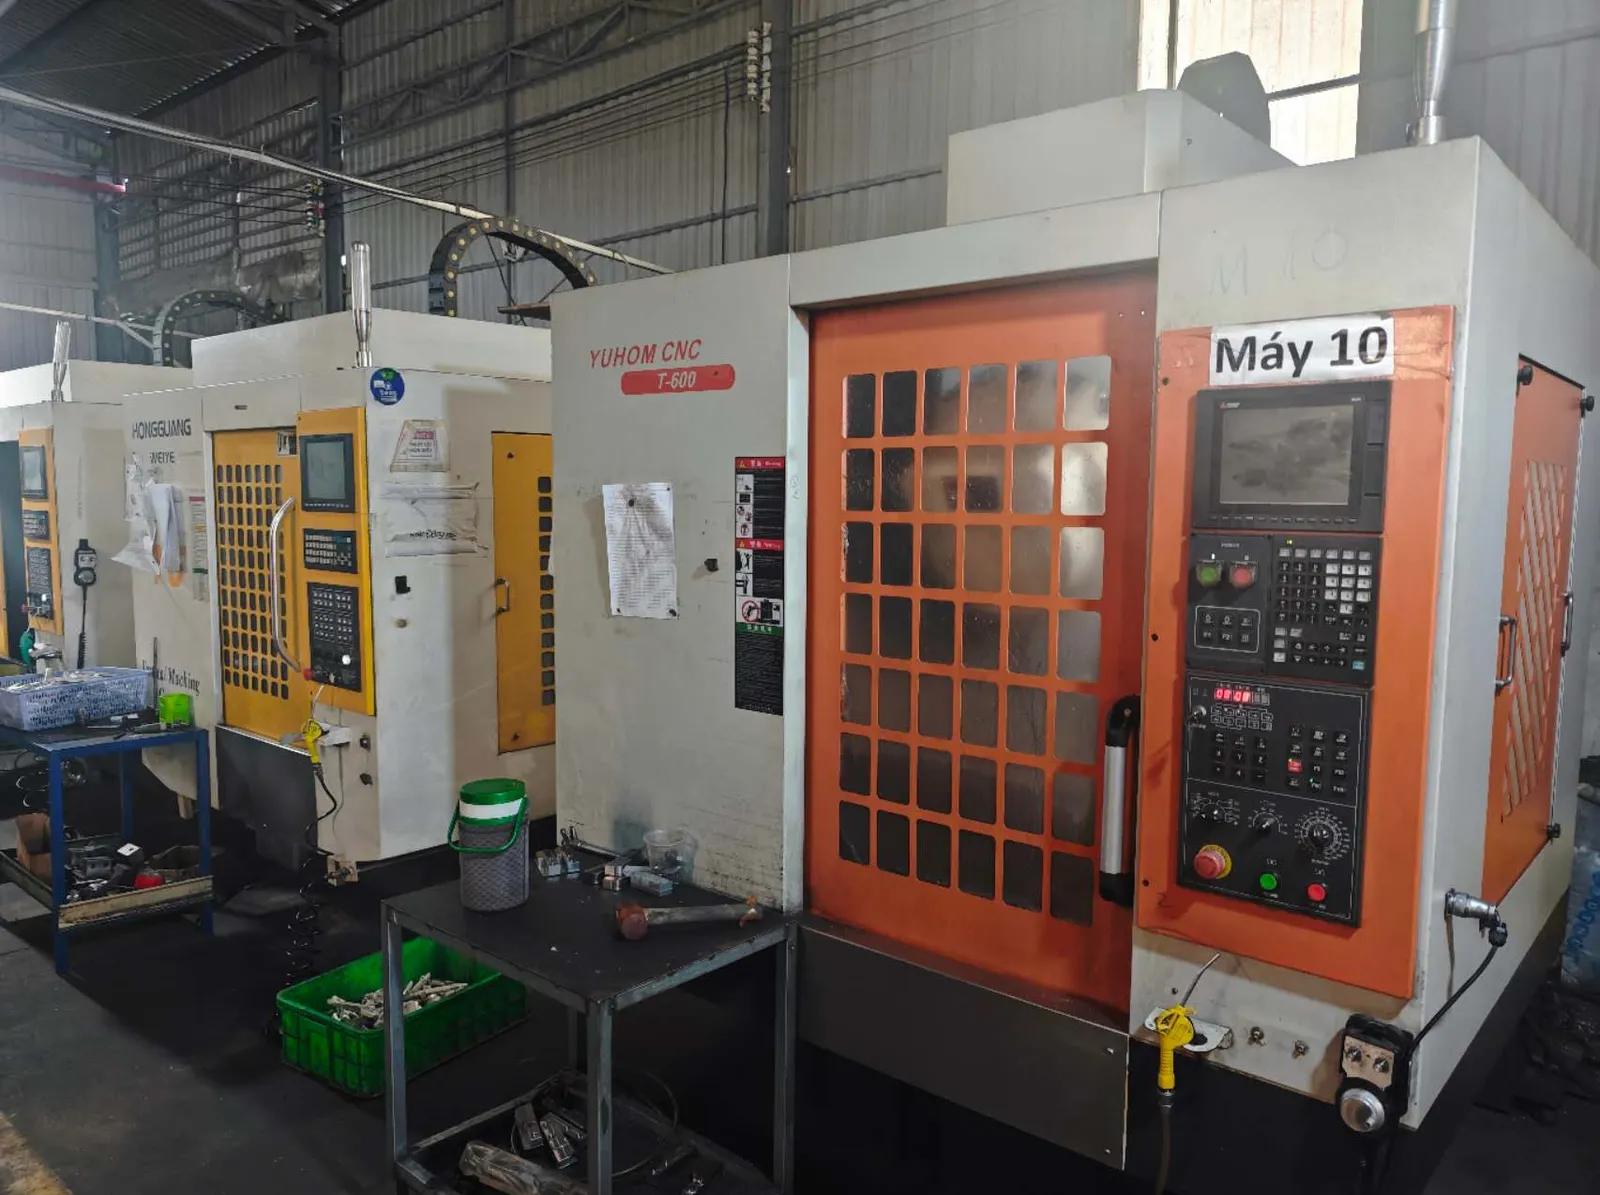
In-house means the lead plant's machines and people: 12 machining centers and 9 CNC lathes, with EDM, welding and polishing alongside. Every card below is a process that plant actually runs.
In-house · our lead CNC plant
Bar and tube work on CNC lathes: bushings, caps, inserts, shafts, knurled and threaded features.
ANPT/NPT to ASME B1.20.1 · knurling
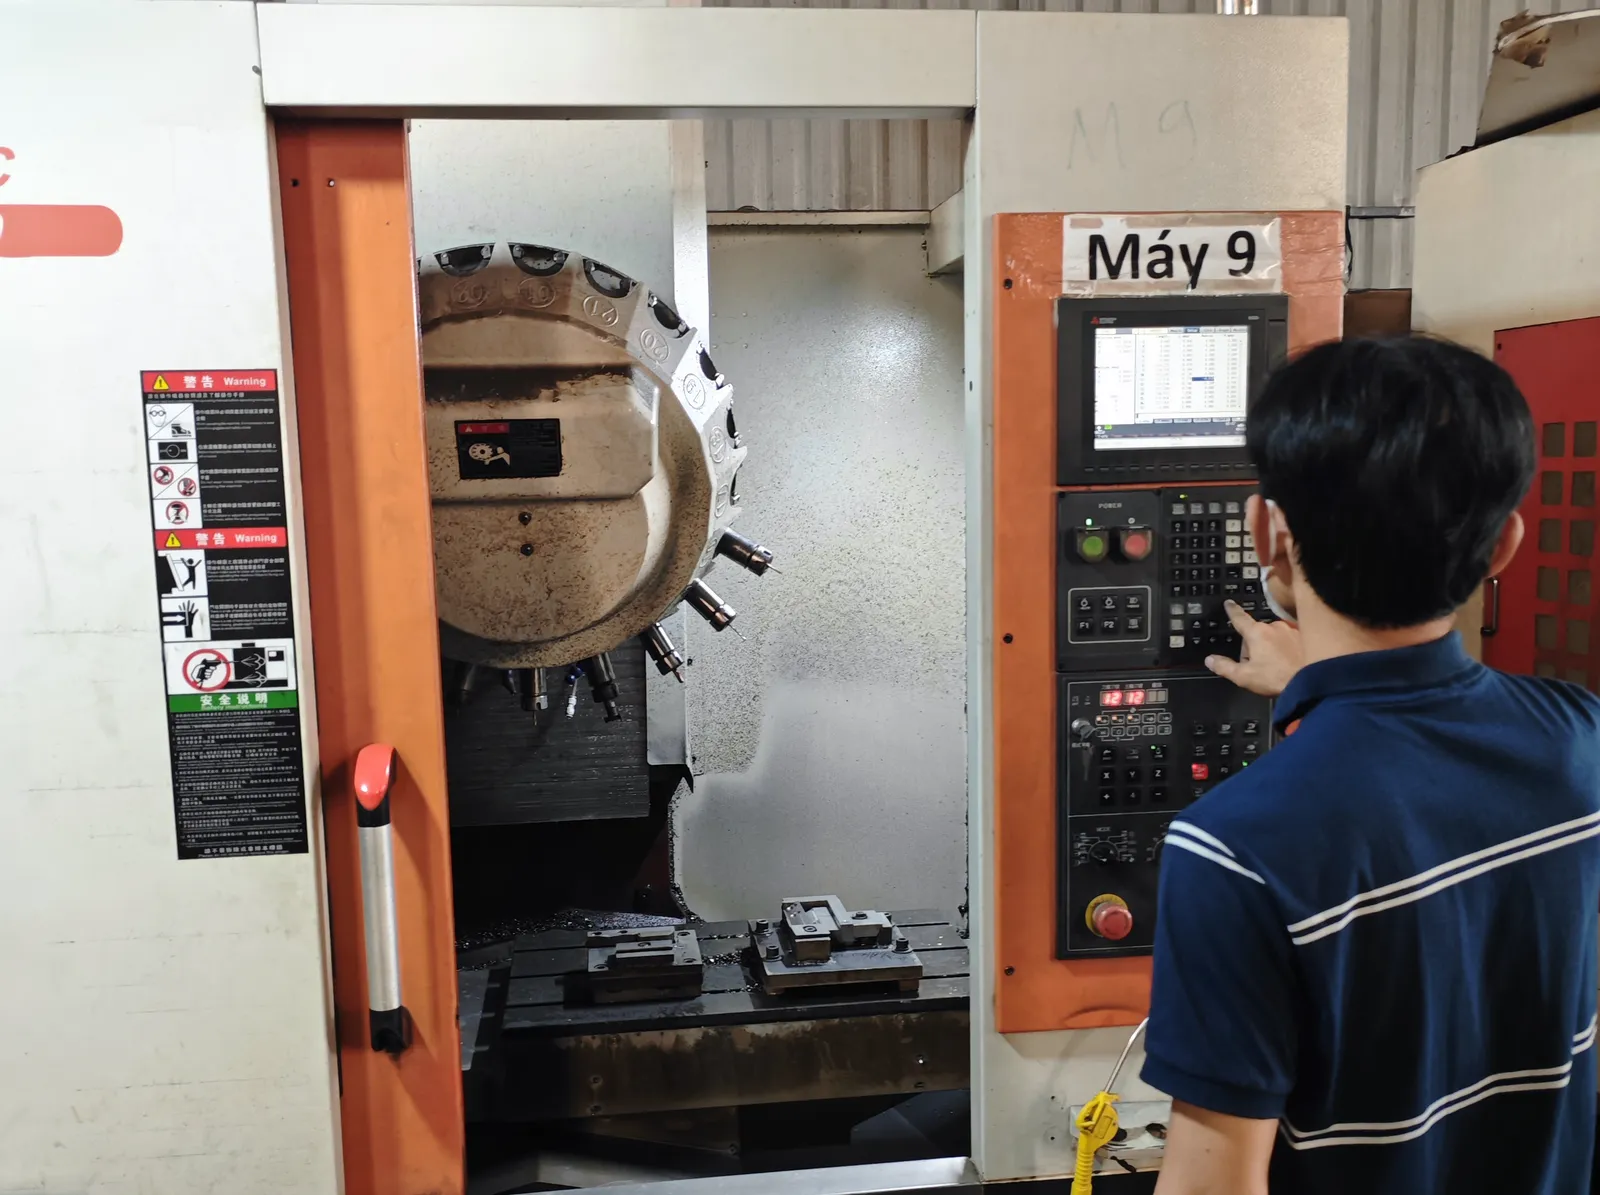
Secondary machining on castings and blanks — datum faces, bores, pockets and tapped holes held to geometric tolerance.
±0.001 in. (0.025 mm) bores · GD&T to Ø0.003 in · 125 RMS
03 — What we coordinate for you
We hold the drawing, the purchase order and the incoming inspection. The work itself happens at a partner's plant, not ours — we say so on every card.
Managed · partner plants we audit and manage
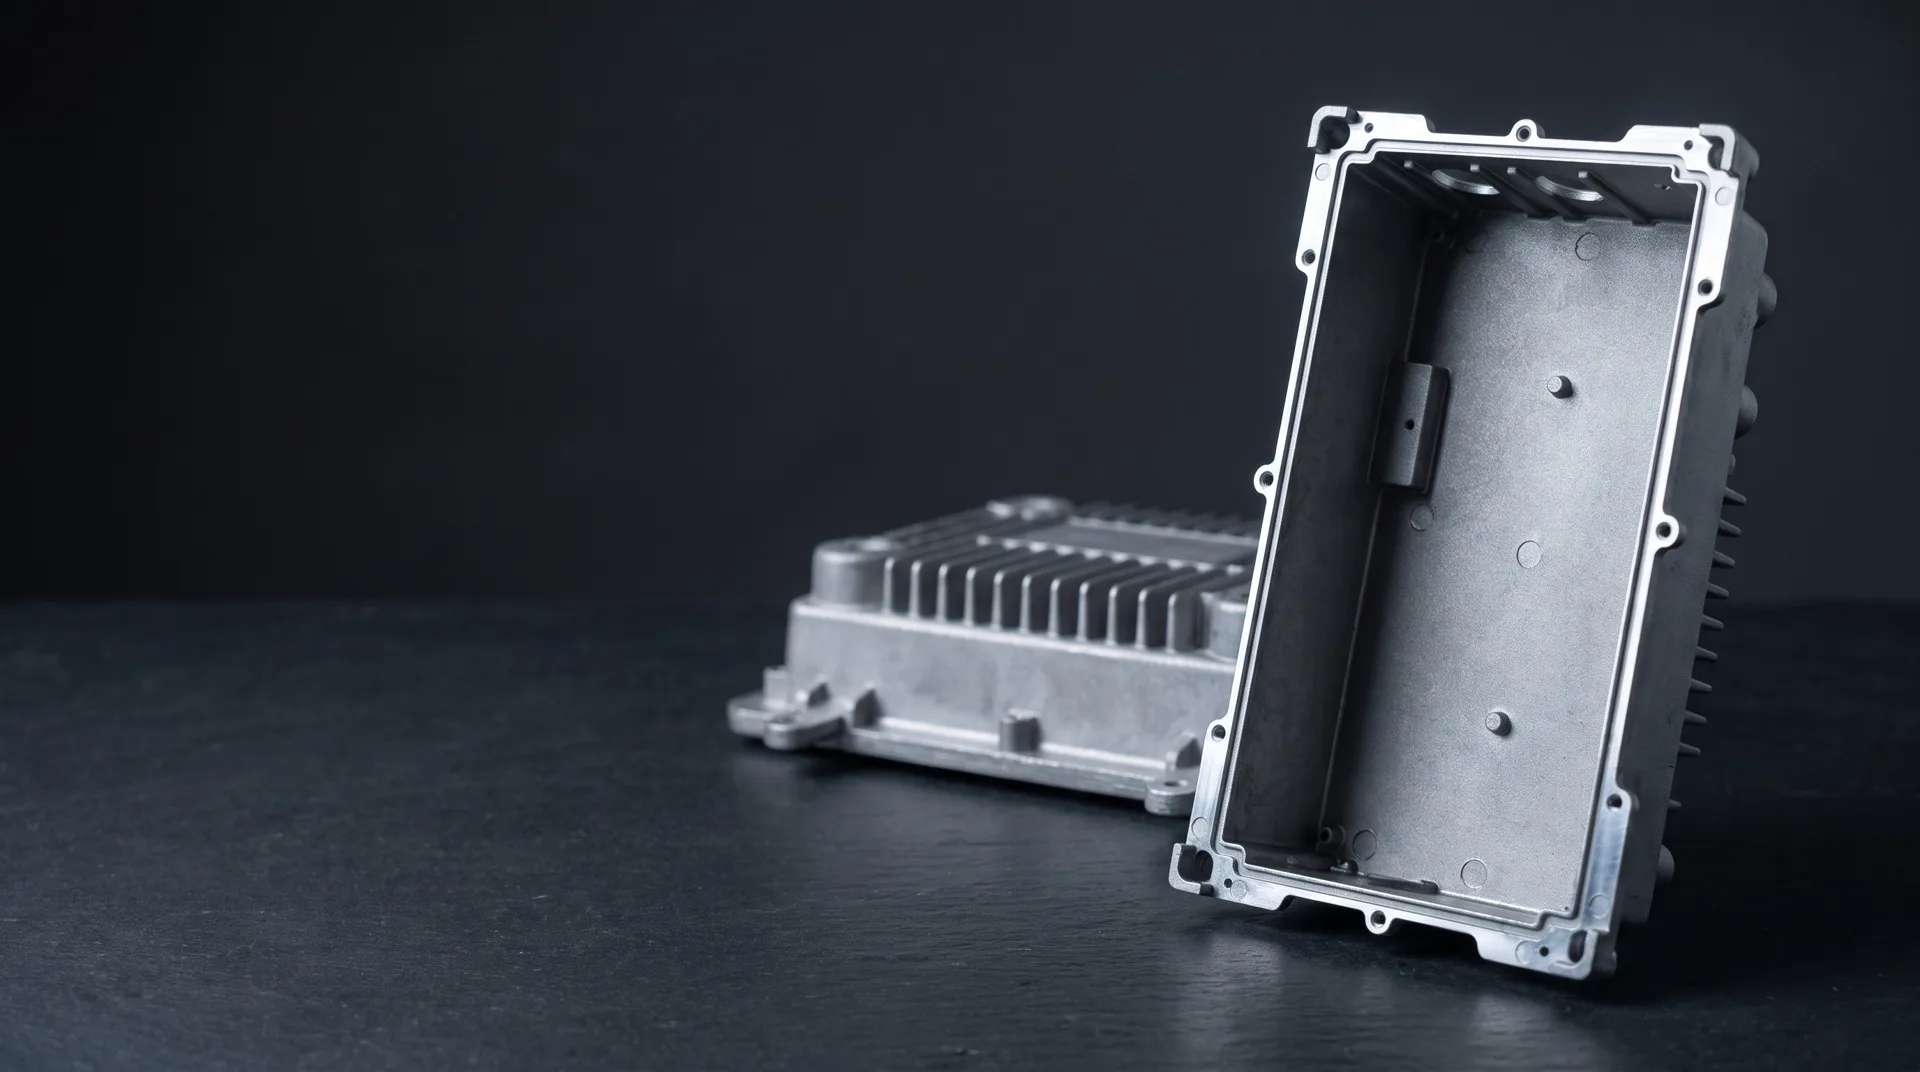
ADC12 aluminum and Zamak 3 zinc, from housings and bases to covers and lamp heads. Cast by partner foundries on production tooling; tooling ownership is set in the quote.
Tooling cost and MOQ set per part in the written quote
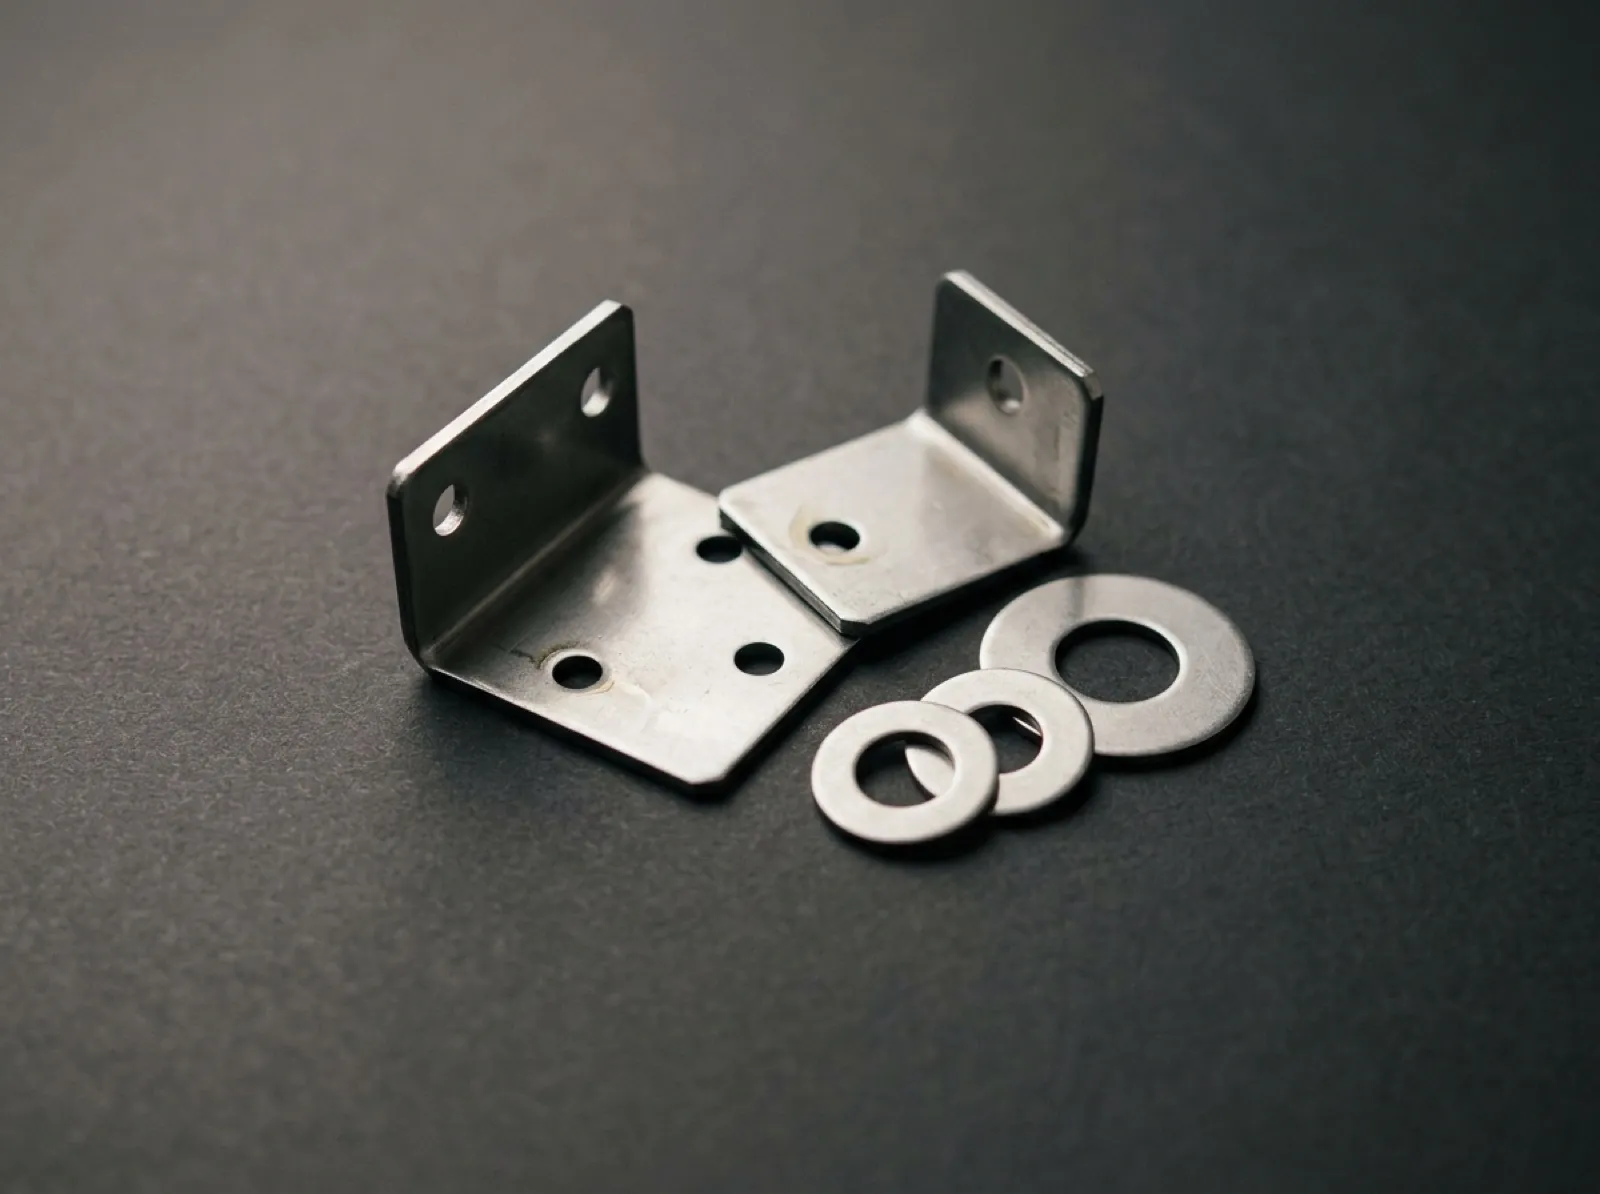
Sheet and strip parts — blanking, forming, piercing and coining. Brackets, washers, clips and plates, pressed by partner stamping plants.
Progressive and compound dies · deburred, oiled, packed
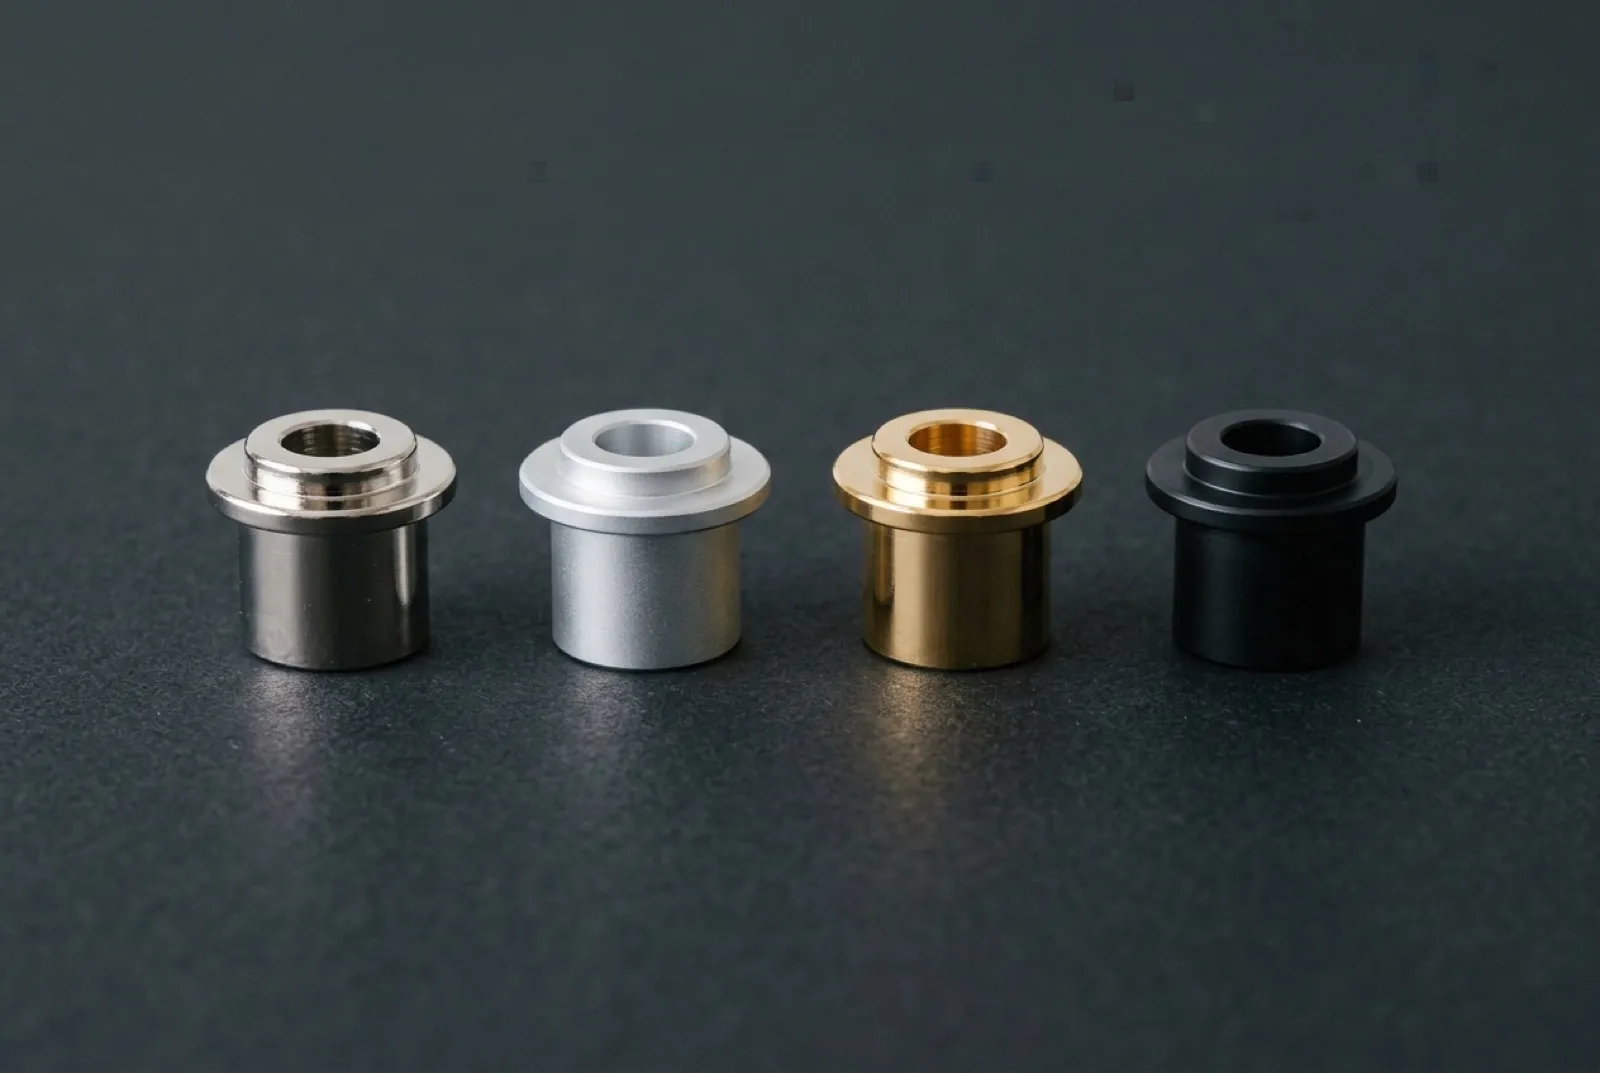
Electroplating, anodizing, gold plating, zinc plating, RoHS trivalent chromate and powder coating with pad printing, applied by partner finishing plants we manage.
Salt-spray results on request · RoHS conformance · cosmetic criteria to print
Brass and bronze bodies poured by a partner foundry we manage. We hold the pattern, the drawing and the PO, then machine and gauge the casting at our lead CNC plant.
Casting managed · machining and thread gauging in-house
Small stainless and steel parts by metal injection molding, and sintered gears, cams and bushings by powder metallurgy, from a partner plant we manage in Vietnam. For high-volume part numbers.
Molding and sintering managed · CNC finishing to print
Profile programs placed with a partner extruder. We hold the drawing, the purchase order and the incoming inspection.
Quoted as a managed program, not an in-house process
Plastic parts and over-molded assemblies placed with a partner molder, so a mixed metal-and-plastic assembly still ships on one PO.
Quoted as a managed program, not an in-house process
Laser-cut, formed and welded fabrications placed with a partner shop and inspected to your drawing before it ships.
Quoted as a managed program, not an in-house process
Thick-plate and heat-sensitive profiles placed with a partner cutter when a part is wrong for laser or stamping.
Quoted as a managed program, not an in-house process
Hollow plastic bodies and tanks placed with a partner molder for programs that pair with our metal components.
Quoted as a managed program, not an in-house process
04 — Where we are
Our lead CNC plant sits in the industrial belt north of Ho Chi Minh City, close to the container port most of our FOB shipments move through.
That proximity keeps trucking short and inland transit predictable, which is part of what a lead time quote is built on. We haven't published exact distances or transit times — we would rather quote a lead time against your specific part and process than hand you a generic number.
05 — One program, start to finish
A real request for an aluminum die-cast base carrying 25 drilled and tapped holes. The customer and the drawing stay under NDA. Everything below is the plan we sent back with the quote: the tool, the fixtures, the finishing and the inspection. The casting and its tool come from a partner foundry; drilling, tapping and the inspection plan run at our lead CNC plant.
ADC12 aluminum from a two-cavity tool, parting line and ejector positions agreed with you before we cut steel.
25 holes per part on four dedicated CNC fixture sets, two parts per fixture.
Casting flash and drill burrs removed by hand at the bench.
The whole part tumbled in a magnetic finisher, which reaches burrs inside small holes that a hand tool cannot.
Ultrasonic wash, then oven-dried, so no chips or coolant ride along in the carton.
Bagged one by one, six to a layer, ten layers to a carton.
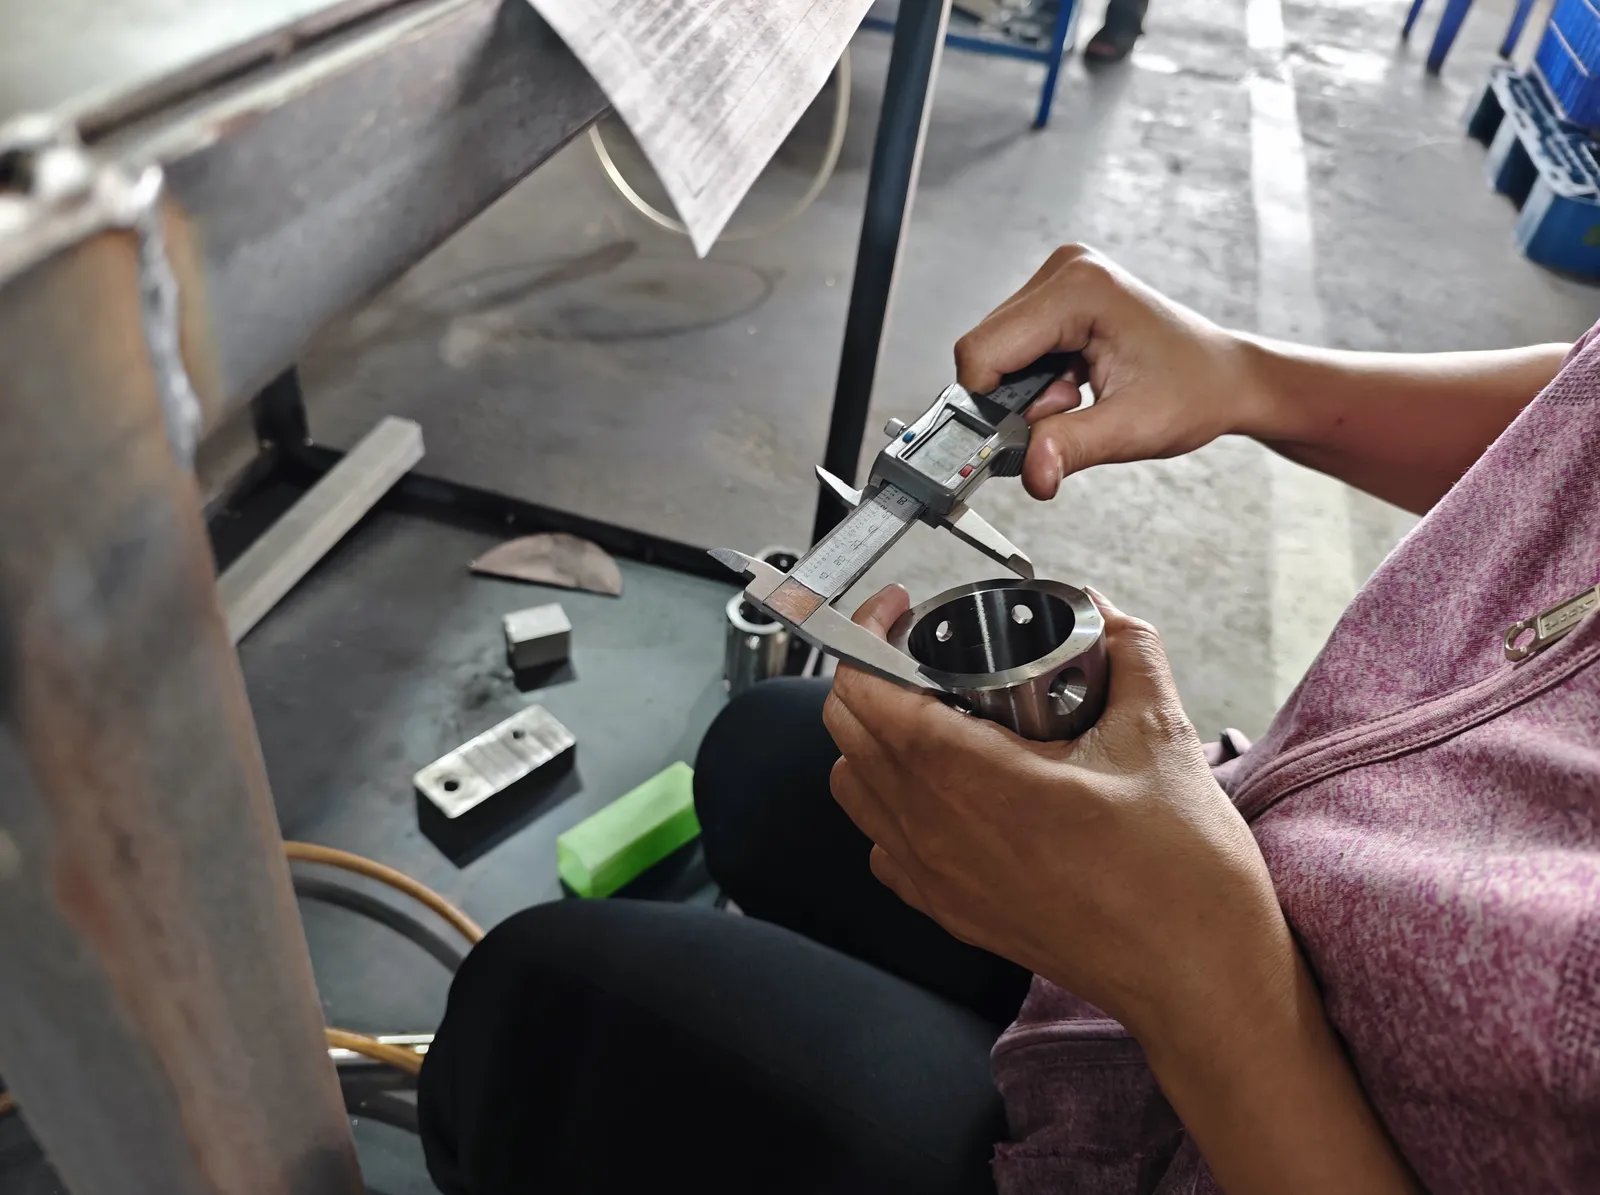
Fourteen features, split by where the risk is. Everything is checked on the first article. Machined holes are checked on every part, because a drill can wander on any cycle. Cast features are checked every two hours, because they only move when the tool wears.
| Feature | Requirement | Method | When |
|---|---|---|---|
| Drilled holes, locating | Diameter ±0.10 mm, depth to minimum | Go/no-go pin gauge, caliper | First article + every part |
| Drilled holes, mounting | Diameter ±0.05 mm, depth to minimum | Go/no-go pin gauge, caliper | First article + every part |
| Cast heights and steps | ±0.10 mm | Caliper | First article + every 2 h |
| Flatness | 0.4 mm | Surface plate | First article + every 2 h |
| Cast bosses and bores | ±0.10 to ±0.20 mm | Caliper, dedicated fixture gauge | First article + every 2 h |
| Tapped holes | Thread size and full depth | Screw run-in to depth | First article + every 2 h |
06 — What the floor actually looks like
No stock photography and no stand-ins. Every photograph in this grid is of our lead CNC plant's floor, machines and parts, unedited apart from cropping and resizing.
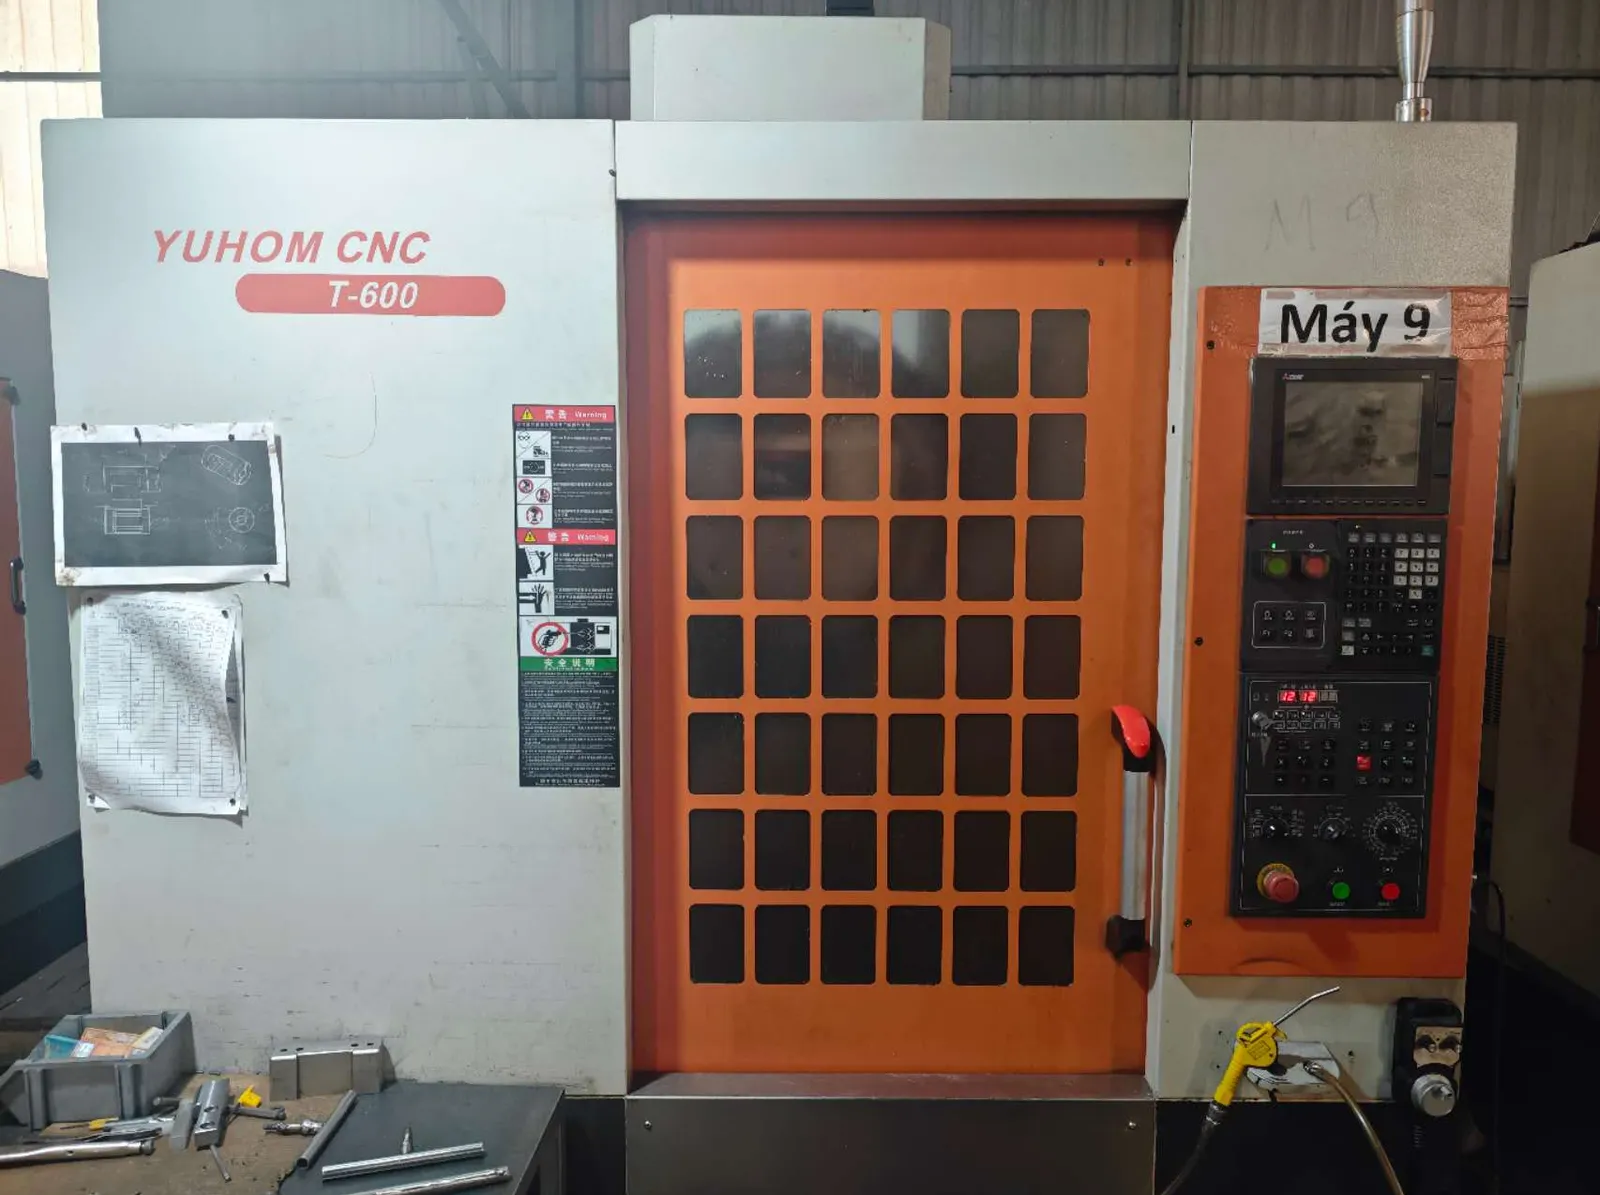
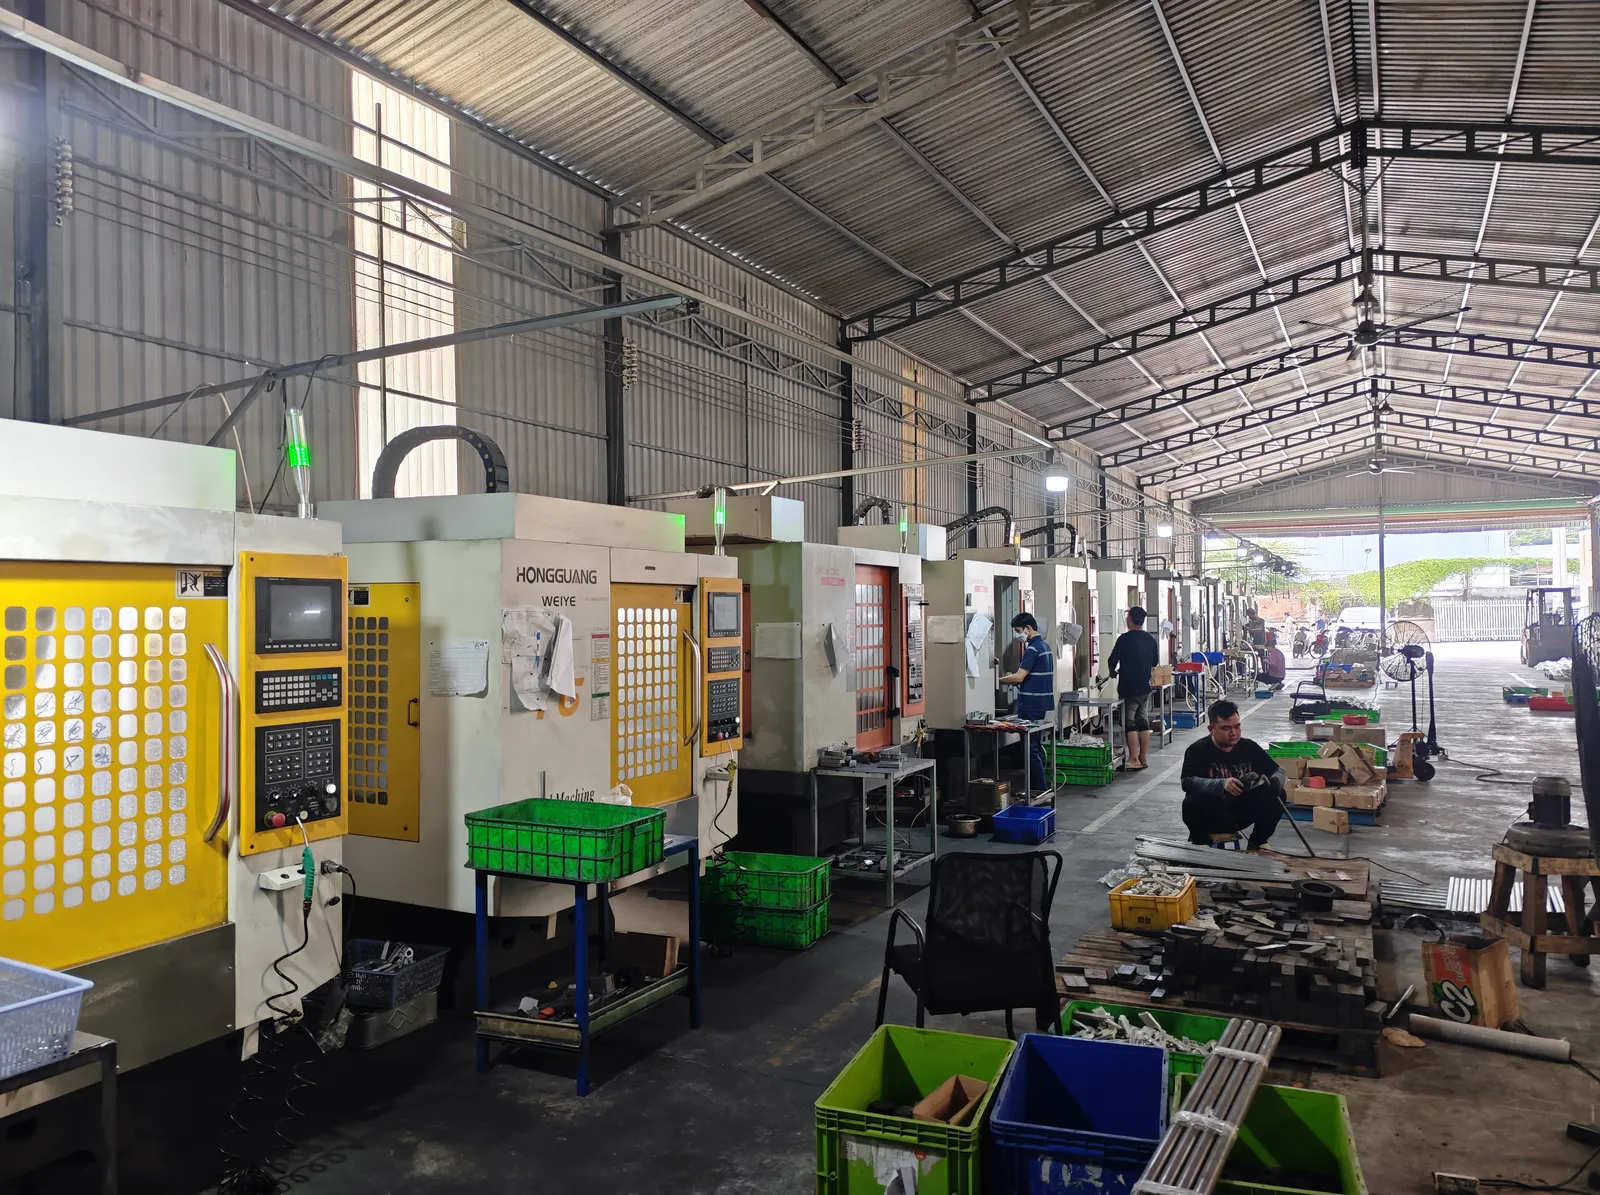
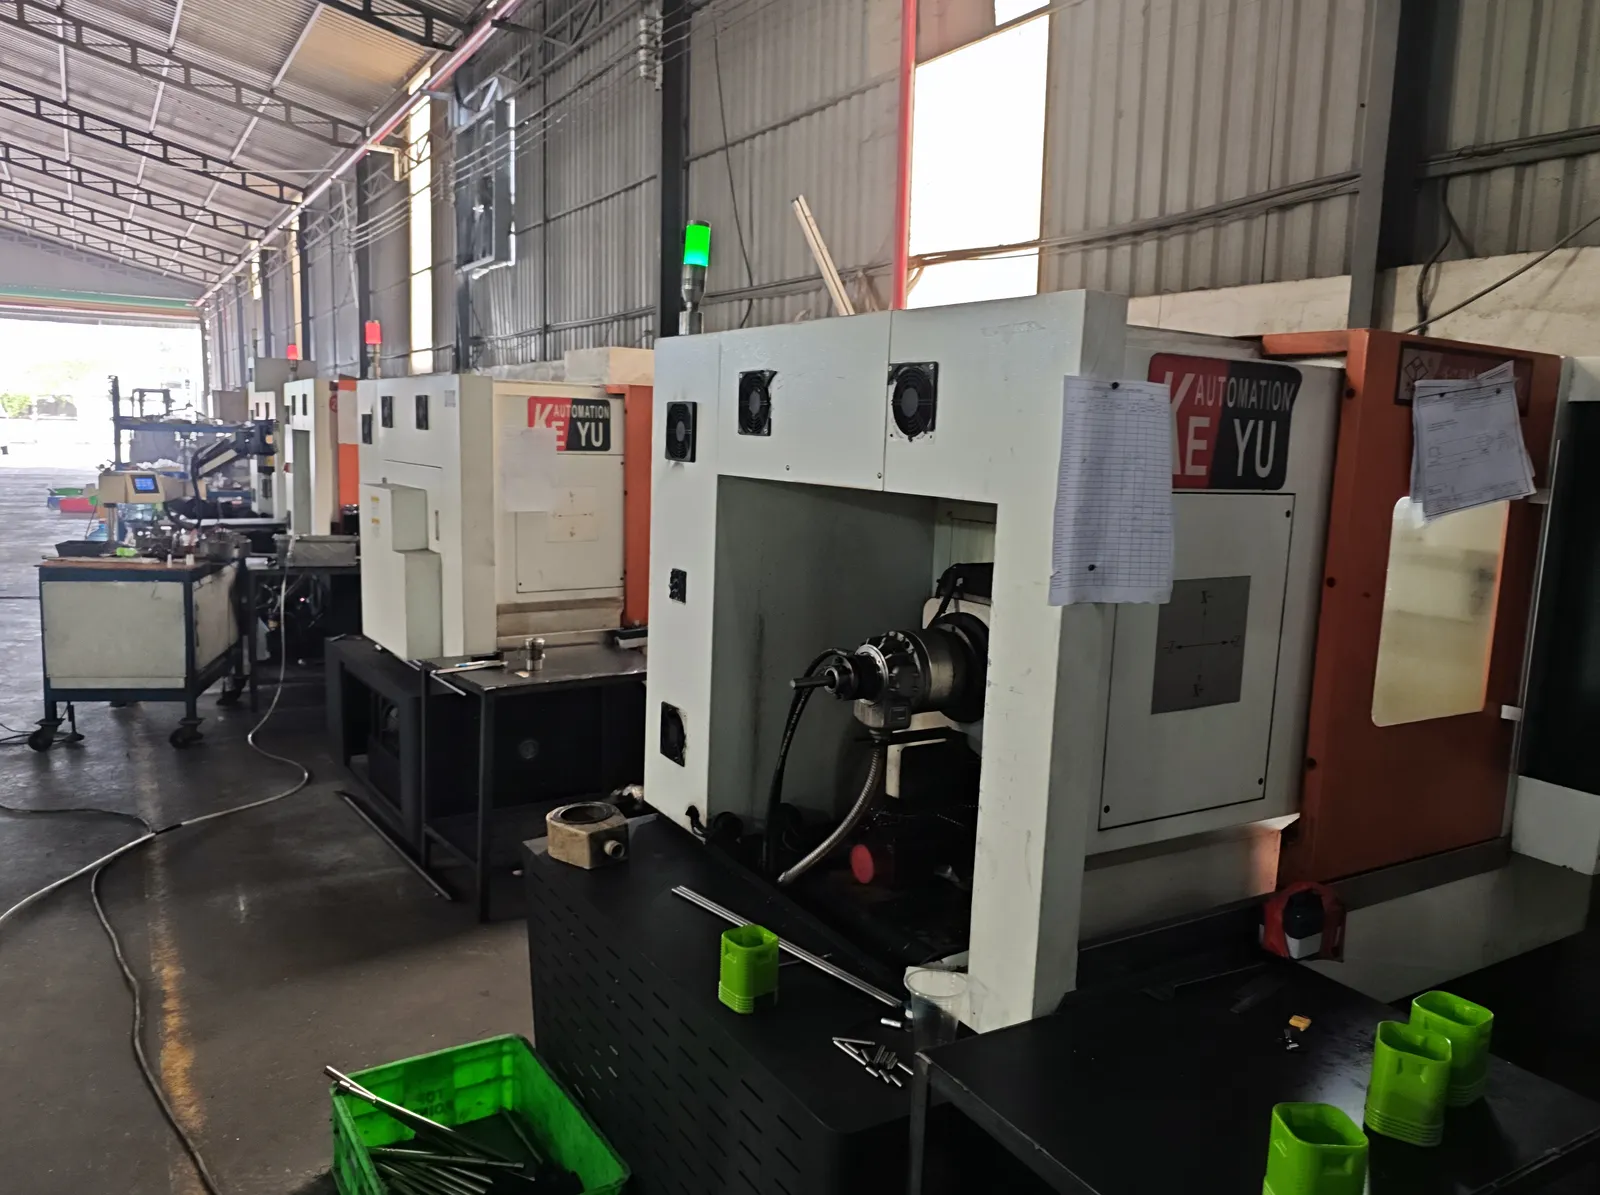
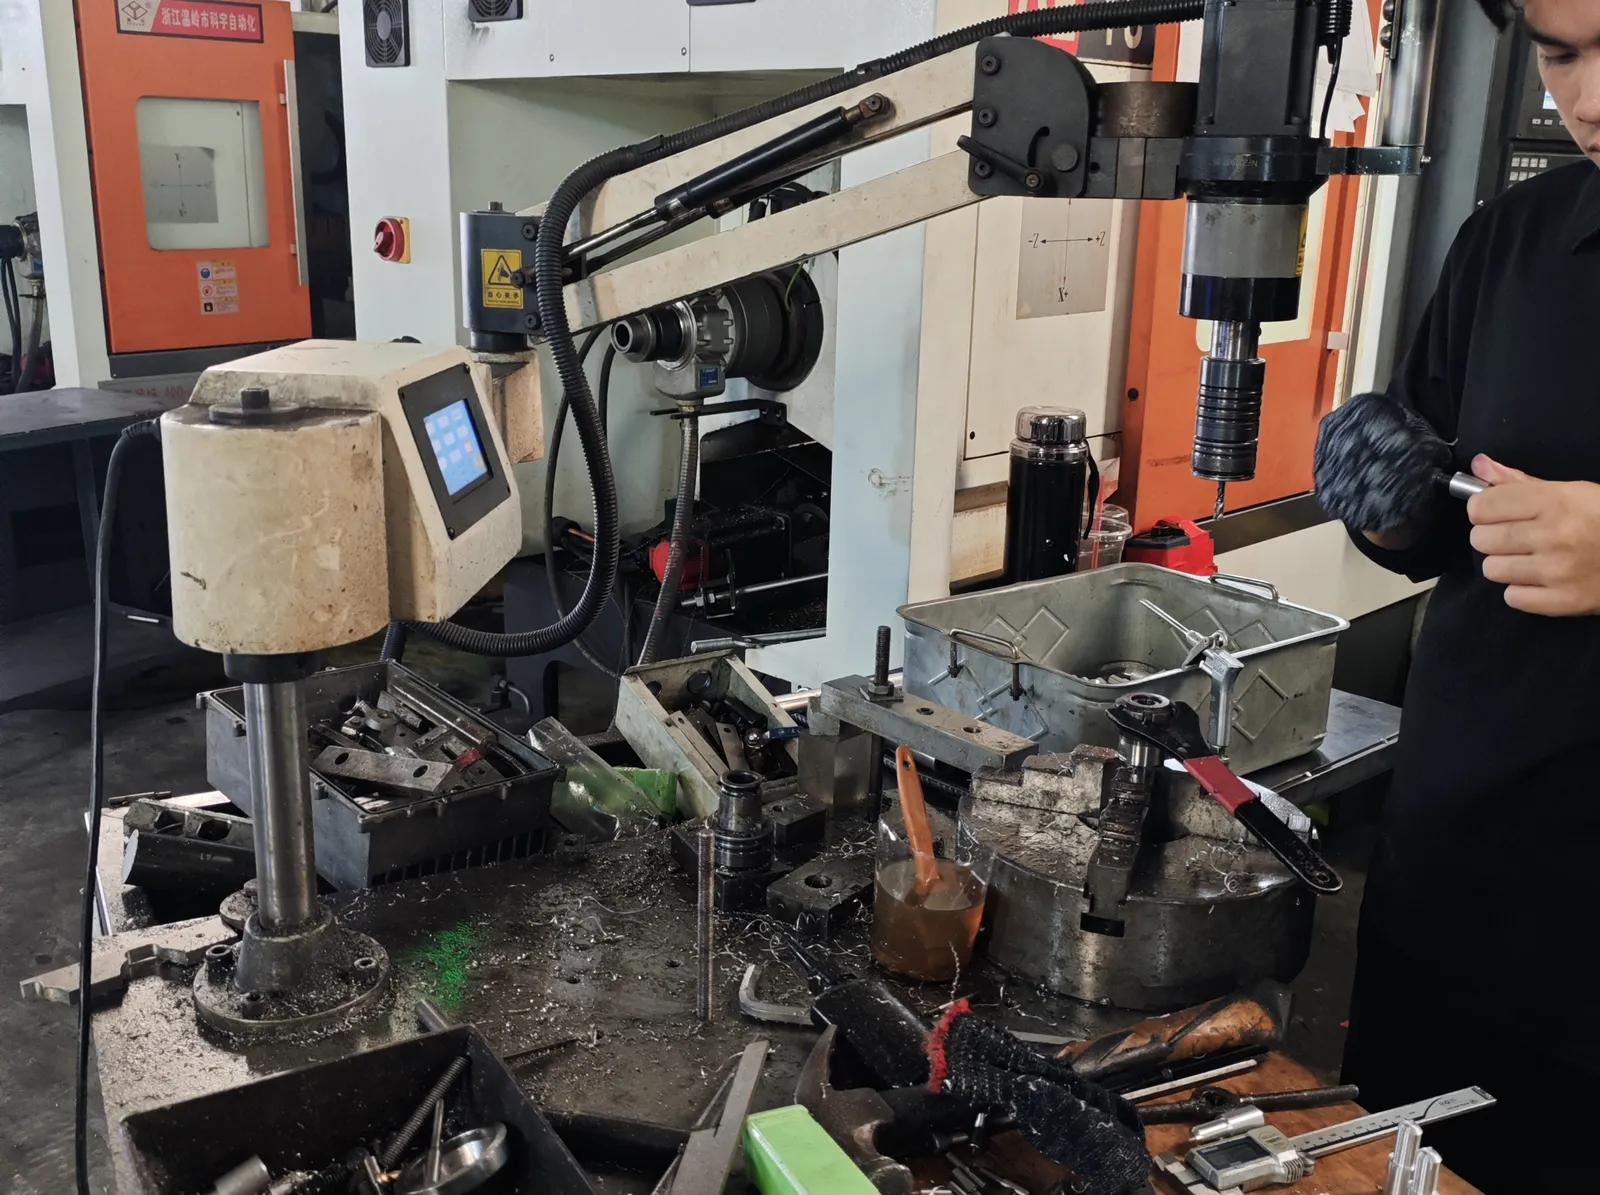
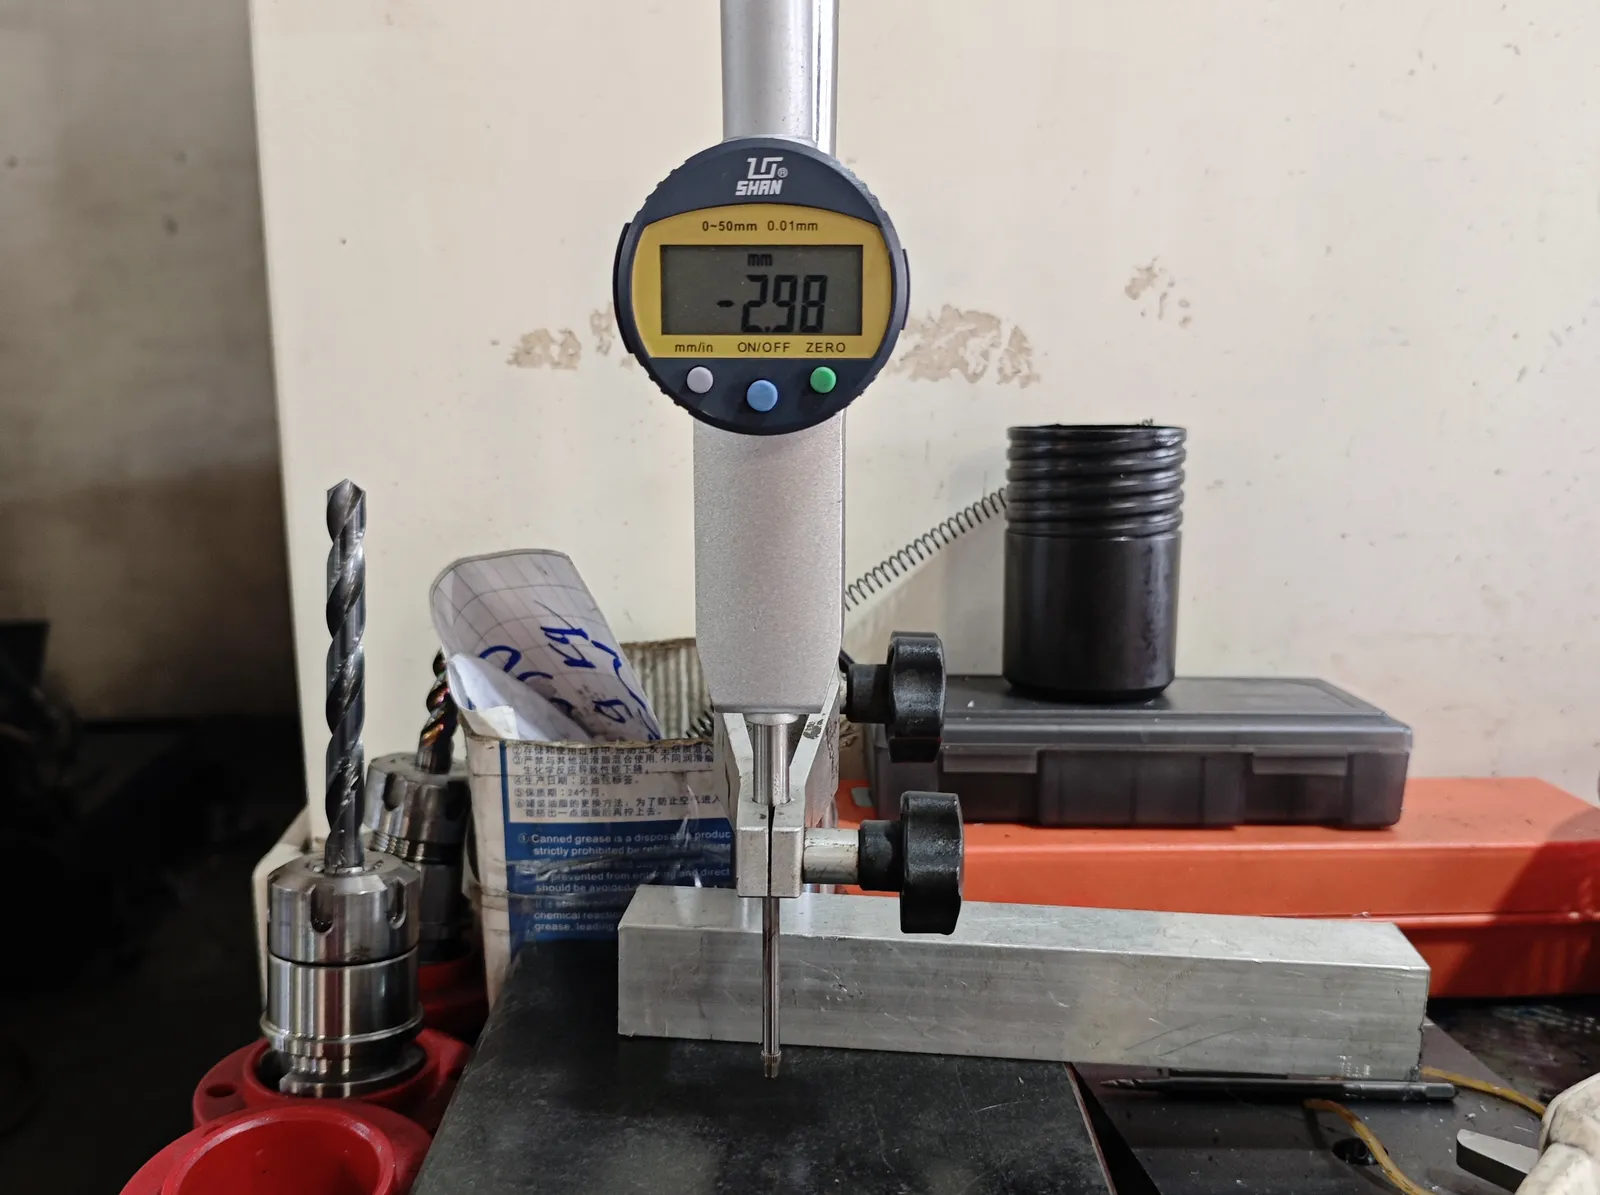
Photos of our lead CNC plant's floor, unedited apart from cropping and resizing. Part and process images elsewhere on this site are illustrations, not photographs.
07 — Come and see it
We are about 45 minutes by car from Tan Son Nhat International Airport (SGN). Send us your flight and we will pick you up at arrivals, walk you through the lead CNC plant, and drive you back.
Can’t fly out yet? We will walk the floor with you on a live video call, on your schedule: the machines, the inspection bench, the packing line, and your part on the machine if it is already running. No slides, no edited footage.