
Metal stamping · Partner plants we manage
Metal stamping managed from Vietnam: sheet and strip parts, blanked, formed and pierced at partner plants.
Saola Manufacturing places brackets, washers, clips and plates from strip and sheet with partner stamping plants it manages, on progressive and compound dies built for your part, and runs the order under one PO. The quote names the production site and country of origin. Deep-drawn shells are outside the stamping work we place.
- Hours
- 48
- Quote returned from your drawing
- Operations
- 4
- Blanking, forming, piercing and coining
- Purchase order
- 1
- Stamping, finishing and any machining together
- Die types
- 2
- Progressive and compound, built for your part
01 — What we actually run
Flat and formed parts, made fast, made flat.
Stamping is the right process when a part is thin, repeatable and made in real volume. Deep-drawn shells are outside the stamping work we place; heavy-plate profiles go to a managed laser/waterjet partner.
Typical parts
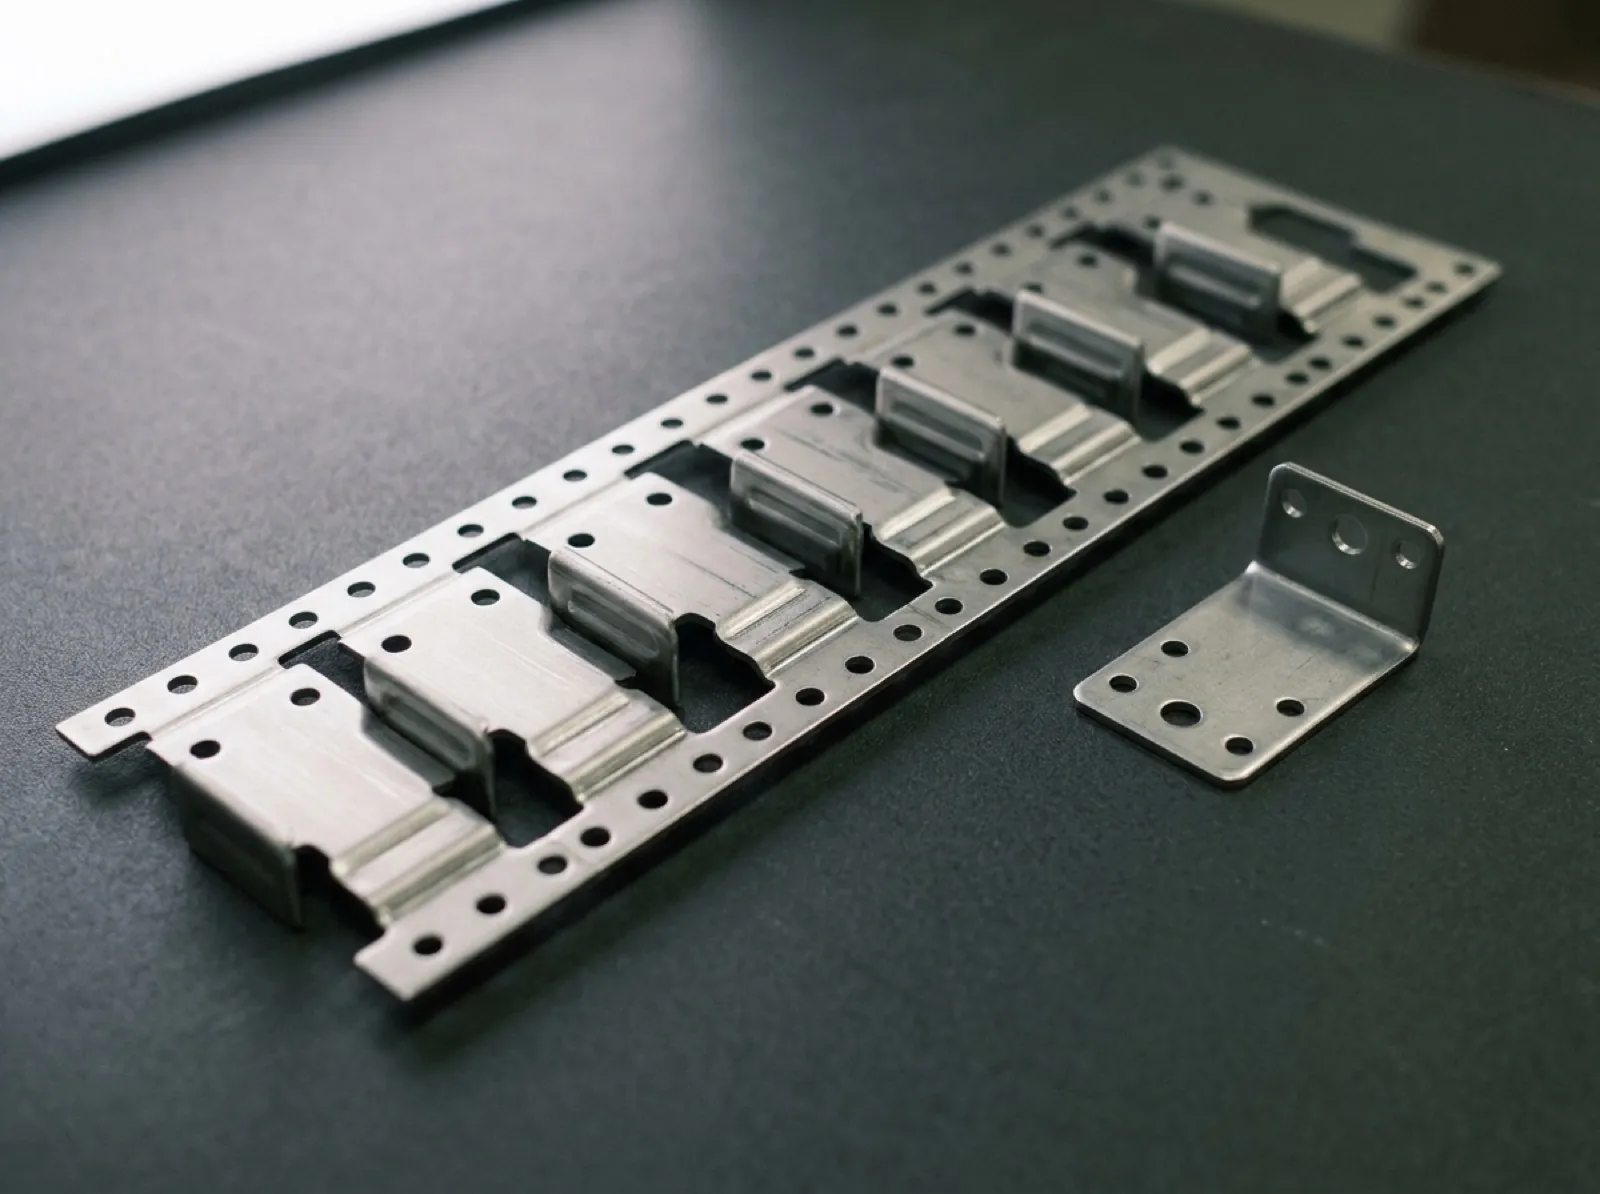
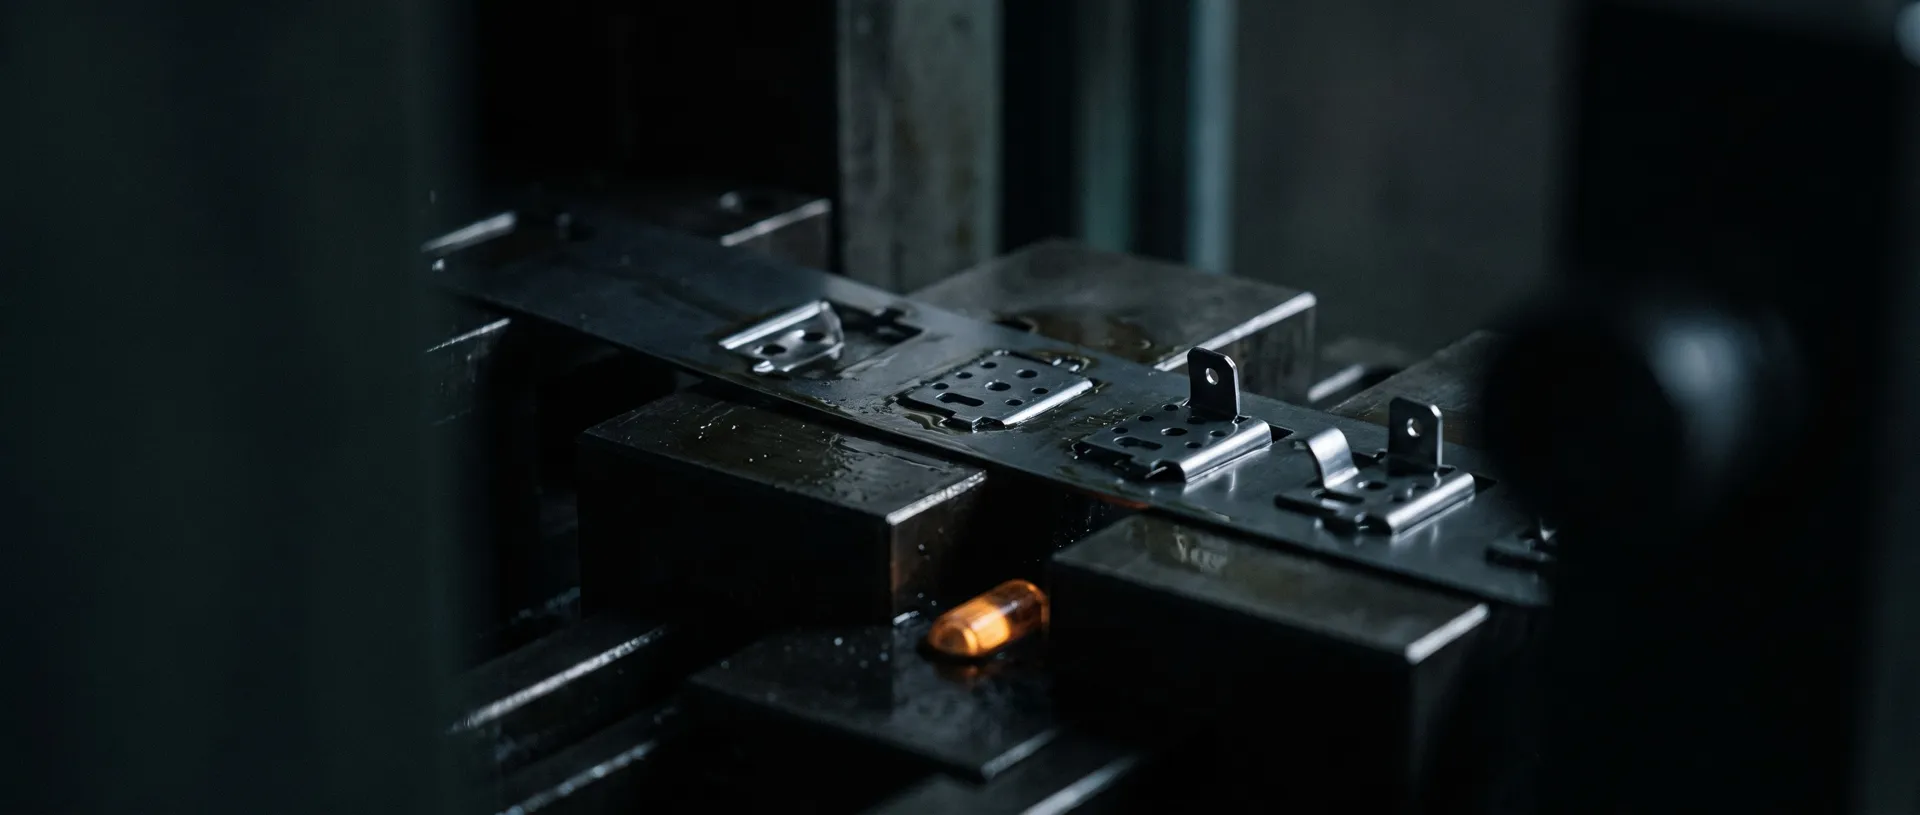
Brackets, washers, clips and mounting plates. Progressive dies run a family of parts through blanking, piercing and forming stations in a single strip pass; compound dies cut and form a simpler flat part in one hit when the geometry allows.
Our partner plants run brass strip and 6061-T6 aluminum sheet routinely, plus steel stampings specified to your drawing gauge and grade.
Low volume, or a design still changing? The break-even between stamping and laser cutting shows where a stamping die starts to pay for itself. Stamping 6061-T6 aluminum? Read bend radius, burr and die rules for aluminum stamping.
Stamped parts by industry: structural brackets for machine tool and industrial equipment, and hinges, latches and mounting brackets for medical and lab cabinetry. Moving a stamped part out of China? Read how US tariffs and country of origin apply to metal parts.
02 — Process parameters
Operations, tooling and materials.
What we build the die around, and what leaves the press.
| Parameter | Specification |
|---|---|
| Operations | Blanking, forming, piercing, coining |
| Tooling | Progressive and compound dies, set and run at partner stamping plants |
| Tooling investment | Set per part in the written quote, depending on station count and complexity |
| Minimum order quantity | Set per part in the written quote |
| Materials run | Brass strip · 6061-T6 aluminum sheet · steel to drawing specification |
| Standard finishing after stamping | Deburred, oil-dip rust protection, zinc plating, RoHS-compliant blue trivalent chromate, all by partner plants |
| Where each step is done | Stamping at a partner plant · any machining at our lead CNC plant · plating at a partner plant; the quote names the production site and origin |
03 — Take cost out of the drawing
Where stamping cost actually comes from.
Die cost and running speed are set almost entirely by the layout you send us. These are the changes that matter most.
1. Keep hole-to-edge distance at or above the material thickness
A hole punched too close to an edge tears instead of shearing cleanly. Standard practice is to hold hole-to-edge and hole-to-hole spacing at least one material thickness — closer than that adds scrap and slows the die.
2. Radius internal corners instead of leaving them sharp
A sharp internal corner concentrates stress in both the part and the punch. A generous radius extends die life and reduces the risk of a cracked part in the field.
3. Standardize hole sizes across a part family
If three parts in a family each use a slightly different hole diameter, that is three punches instead of one shared punch. Round to a common size wherever the assembly tolerance allows it.
4. Avoid tight flatness on a part that gets formed anyway
A flatness call-out on a part that already goes through a forming station is usually redundant — the forming operation sets the final shape. Save the tight flatness spec for parts that ship flat.
5. Hold one gauge across the family where you can
Every material thickness change is a material changeover on the press. A family that shares one gauge and one alloy runs back to back without a changeover between parts.
04 — Where this is the wrong process
What stamping does not do here.
Not for deep draws or heavy plate
The dies we place are built for blanking, forming, piercing and coining on strip and sheet stock. Deep-drawn shells are outside the stamping work we place; heavy-plate profiles go to a managed laser/waterjet partner, so ask us and we will route the part correctly instead of forcing it onto a die it was never designed for.
On small runs, especially for a multi-station progressive part, the die does not amortize; we are not competitive there and will tell you so on the quote.
05 — One supplier, one PO
A bracket rarely ships alone.
The stamped brackets we manage are usually part of a larger assembly — paired with a cast housing or a turned fastener, finished and packed together under one PO.
Surface finishing
Deburred, oil-dipped or zinc plated by partner plants after the press, on the same part number.
See the finish menuDie casting
A stamped mounting bracket paired with a die-cast housing, shipped as one assembly.
See die castingCNC turning
Turned pins, inserts or fasteners assembled with stamped parts before packing.
See CNC turning
Progressive die or compound die — which do I need?
A compound die cuts and forms a simpler flat part in one station. A progressive die runs a strip through several stations — blank, pierce, form — for a part with more features. We will tell you which one your drawing calls for once we see it.
What materials can be stamped on a Saola order?
Brass strip and 6061-T6 aluminum sheet are what our partner plants run most often. For steel, tell us the grade and gauge on your drawing and we will confirm a partner plant can run it before quoting.
Can stamped parts be finished on the same order?
Yes. Deburring and oil-dip rust protection are standard after stamping, and zinc plating or RoHS-compliant blue trivalent chromate can be added on the same PO, applied by a partner plant and named in the quote — see surface finishing.
Stamping guides
Send a stamping drawing. See the die cost first.
STEP or PDF. You get the tooling investment, a unit price at your volume, the lead time, and a short note on anything we would change to take cost out.