Meter & electronics housings
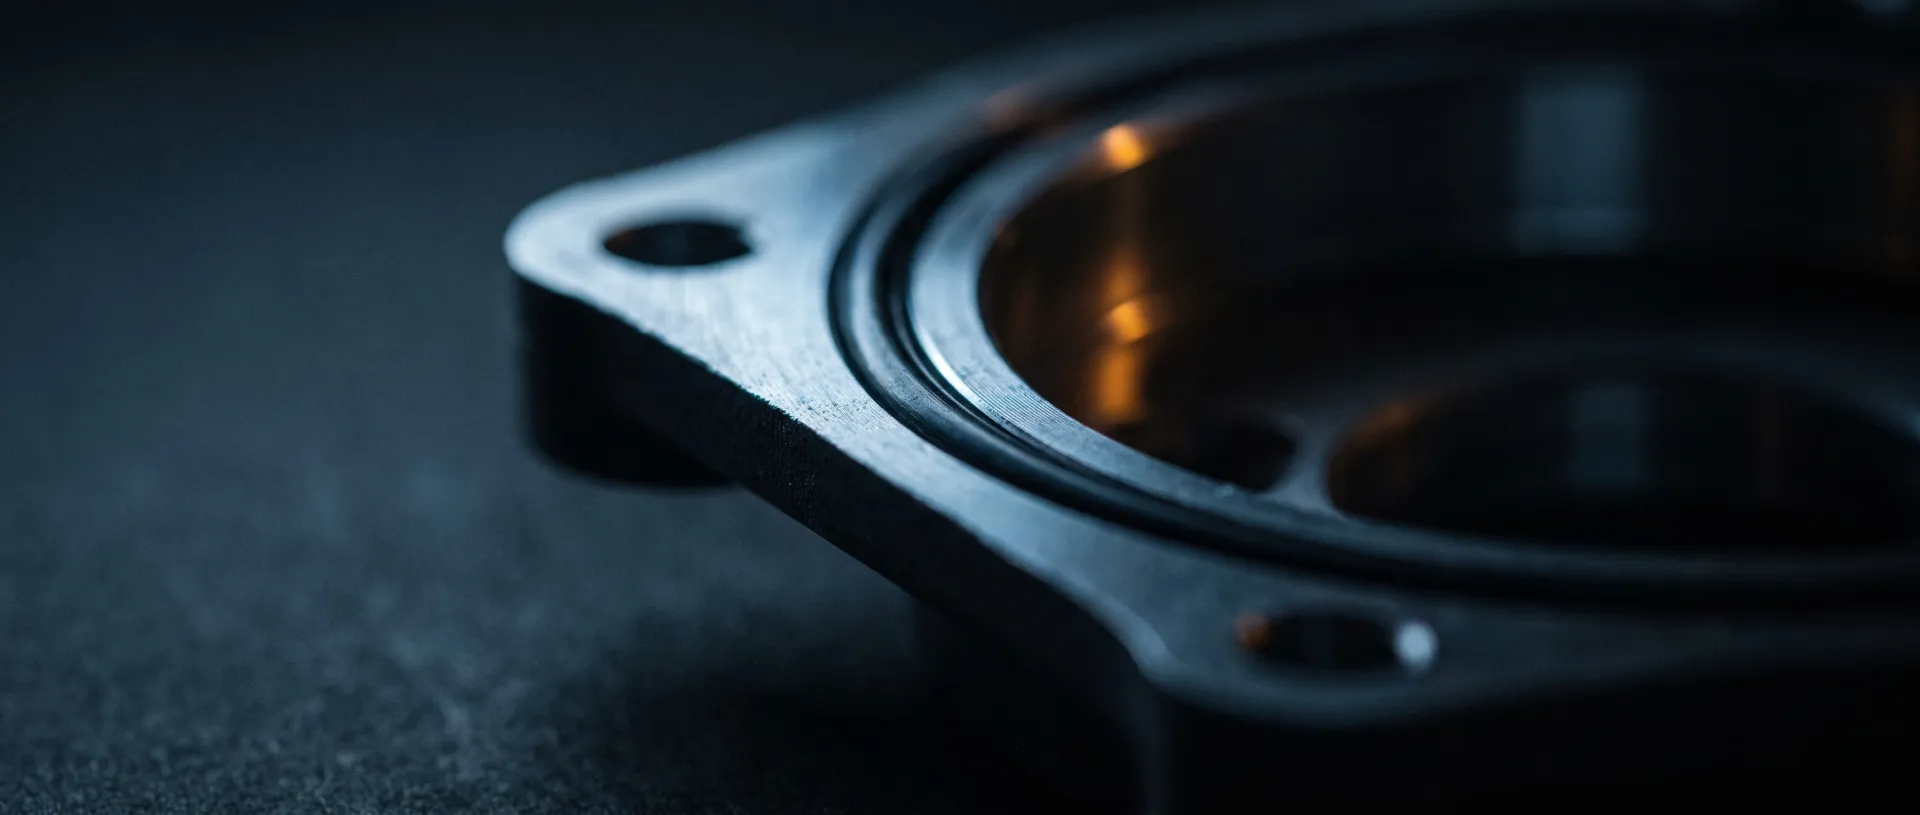
Die cast in ADC12 aluminum, then machined: gasket faces flat to print, cable-entry and port bores, tapped mounting bosses. Powder coat or conversion coat for outdoor service.
Gas & water distribution · Metering and control hardware
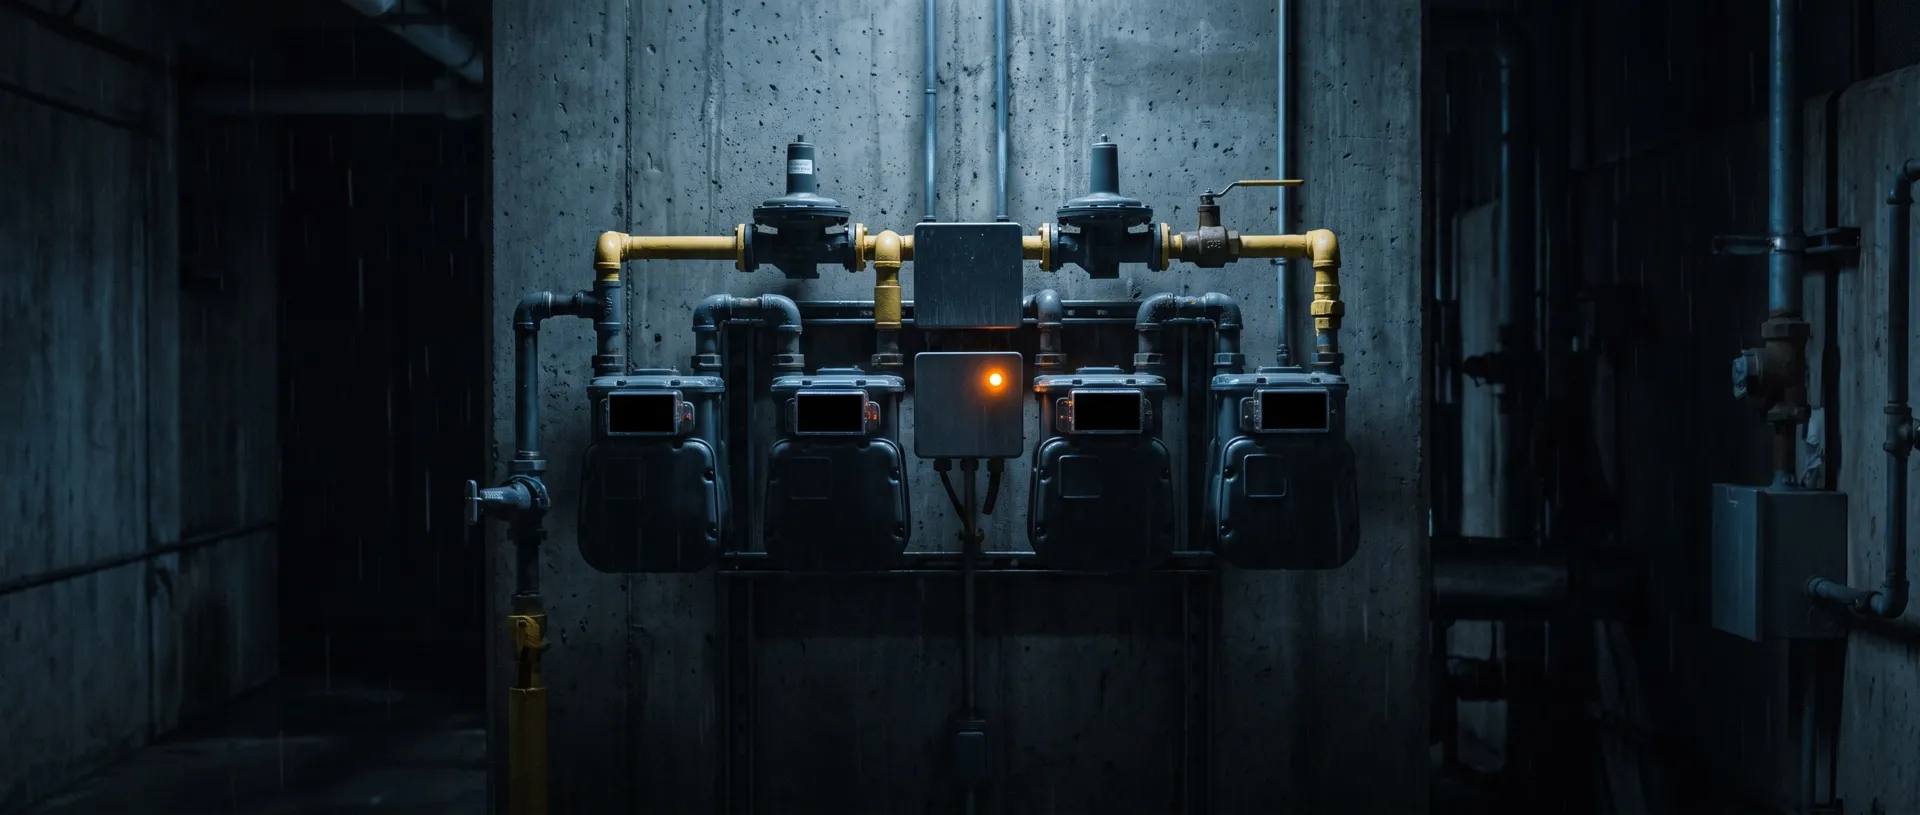
Die-cast and machined housings, sensor and solenoid covers, and valve bodies for gas and water metering and pressure control. The value is in the sealing face, the port thread and the finish, not in the pound of metal, so that is where the machining and the inspection go.
01 — The parts we make for this industry
Housings, covers and bodies are the core of the program. Caps, stems and sleeves ride on the same PO, so the whole assembly ships from one supplier with one inspection standard.
Die cast in ADC12 aluminum, then machined: gasket faces flat to print, cable-entry and port bores, tapped mounting bosses. Powder coat or conversion coat for outdoor service.
Machined from 6061 aluminum: pockets, counterbored fastener holes, clear or colored anodize, sealed. The cover that keeps moisture out of an electronics or solenoid cavity.
Aluminum bodies die cast in-house; brass and bronze bodies poured by a partner foundry we manage. Both bored, faced and threaded ANPT/NPT in our plant.
Die-cast or machined aluminum heat sinks, brackets and mounting plates for the electronics inside metering and control boxes.
Turned in 52100, C1117 or stainless, matched to the body they seal into; threaded inserts and bushings for field-serviceable assemblies.
Turned pipe caps, plugs and DOM-tube stiffeners, quoted as part of a housing or valve program rather than as stand-alone commodity lots.
02 — What actually matters on these parts
None of these are cosmetic. A miss on any one of them is a leak claim, a corroded fitting in the field, or a seal that never sat flat.
ANPT and NPT threads are gauged against that standard, in the same inspection pass that checks bore concentricity and finish. They are not sampled after the fact.
Plated or coated parts are held to 96 hours salt spray. RoHS-compliant blue trivalent chromate zinc plating or oil-dip rust protection is specified by exposure, not by default.
A burr on a thread crest or a gasket face cuts the seal on first assembly. Deburring is checked at the same station as the dimensional inspection, not left to a downstream sort.
Machined bores on castings hold ±0.025 mm with GD&T concentricity to Ø0.003 in. An off-axis bore loads a seal unevenly, and it will weep under pressure eventually.
03 — Typical routing by part family
Process route, material and finish for the part families above. Volumes and exact routing are confirmed against your drawing.
| Part family | Process route | Material | Finish |
|---|---|---|---|
| Meter & electronics housings | Die casting + CNC machining | ADC12 aluminum | Powder coat or conversion coat |
| Sensor & solenoid covers | CNC milling | 6061-T6 aluminum | Anodize, clear or color, sealed |
| Regulator & valve bodies | Die casting, or managed sand casting, + CNC machining | ADC12 aluminum / brass / bronze | Plate or polish, pad print |
| Stems, shafts & inserts | CNC turning | 52100 / C1117 / stainless | Zinc plating or passivation |
| Caps, plugs & sleeves | CNC turning | 12L14 / brass / A513 DOM tube | Zinc, RoHS trivalent chromate or oil-dip |
04 — One part, one supplier
A representative routing for this industry. Every step below happens inside our own plant, from the casting tool to the carton.
ADC12 housing cast to near-net shape from tooling we own and maintain.
Gasket face, cable-entry bores and tapped bosses cut to print in one setup.
Sealing faces and thread crests dressed clean — the step that decides whether it leaks.
Powder coat or conversion coat to the exposure the housing will see, then pad-printed.
Flatness and thread check, individual bagging, cartons under 30 lb.
05 — Where we are the wrong shop
We do not hold NSF/ANSI 61 or an equivalent potable-water contact certification. If your part touches drinking water directly and that approval is required, confirm it with us before tooling. We will tell you honestly whether we can pursue it, or whether you need a different supplier for that part.
We machine and finish the part to your print. We do not certify an assembly for ATEX or a similar hazardous-area rating — that qualification sits with your engineering team at the assembly level.
That is our routine turned-feature tolerance, not our floor for every feature. If a critical bore needs tighter, say so on the drawing and we will tell you plainly if it is outside what we can hold.
06 — Before you send a drawing
Short answers here; the rest on the FAQ page.
ANPT and NPT threads are gauged against ANSI/ASME B1.20.1 limits in the same inspection pass that checks bore concentricity and finish. Tell us your acceptance sampling plan and we will quote against it.
Not today. We do not hold NSF/ANSI 61 or an equivalent certification. If that approval is required for your part, tell us before you send a drawing. We will be honest about whether it is worth pursuing for your volume.
Between 5,000 and 30,000 pieces depending on the process — die casting starts lower, sand casting higher. Below roughly 2,000 pieces we are not competitive and will say so rather than quote badly.
STEP or PDF, one part or a whole family. You get a unit price at your volume, the tooling cost and the lead time, plus a note on the thread and finish callouts. Turnaround is two business days.